20 Verified Before-and-After Industrial SLA & Sculpia Case Studies: Flagship Engineering Hub
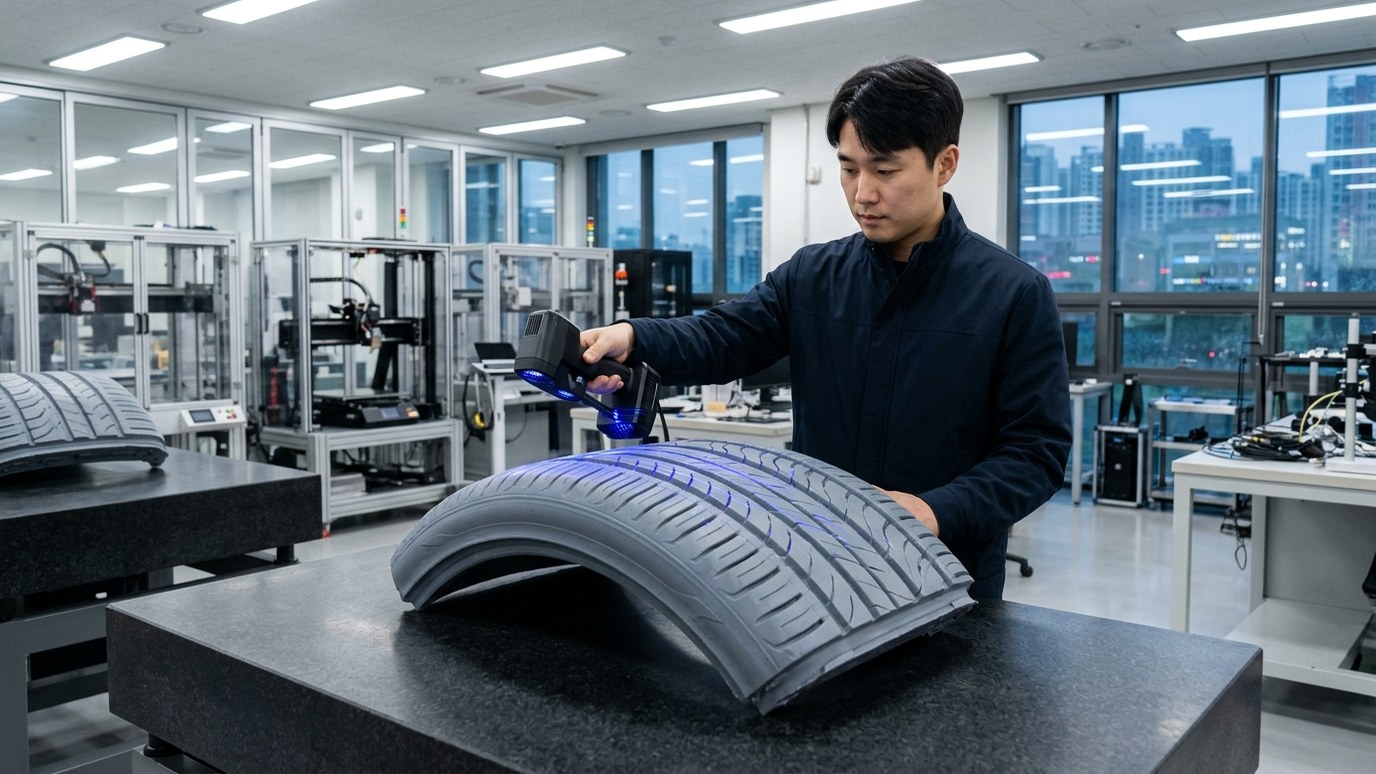
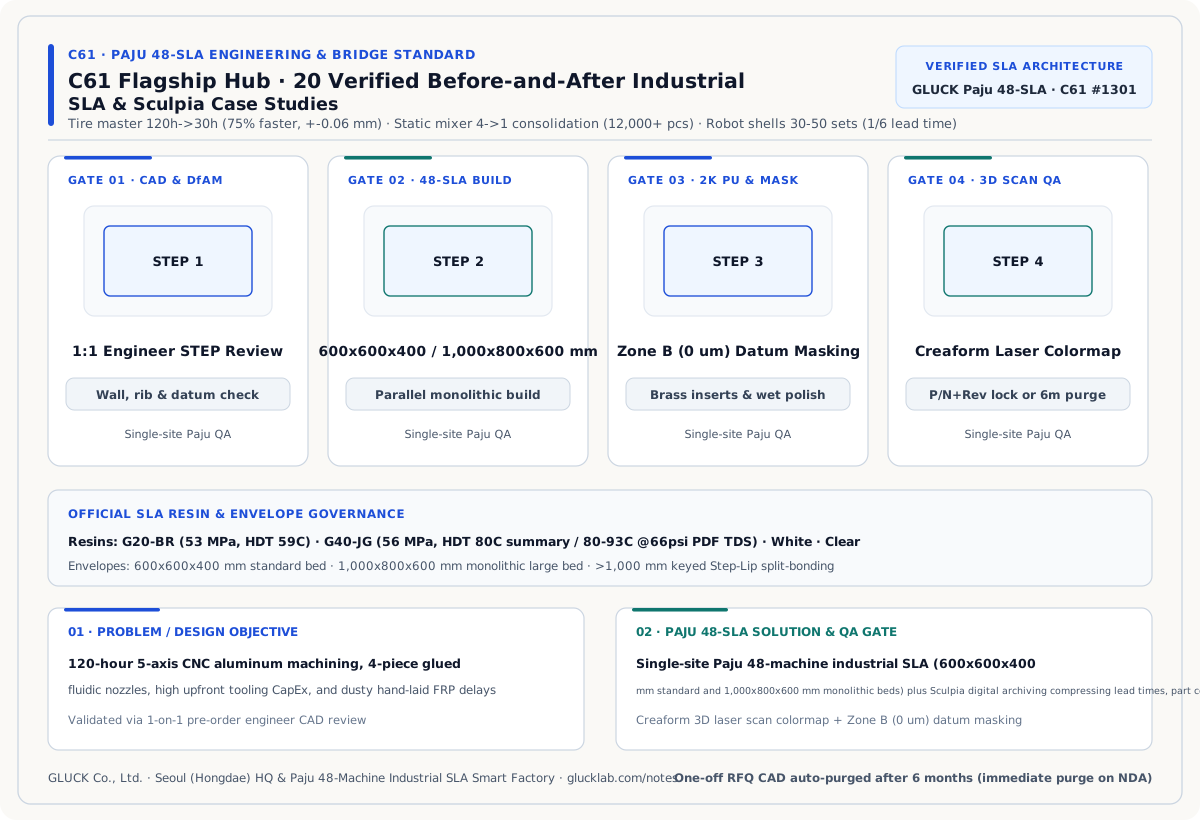
20 Verified Before-and-After Industrial SLA & Sculpia Case Studies: Flagship Engineering Hub — Verified Before-and-After comparison: Tire master 120h to 30h (75% faster, ±0.06 mm) · Static mixer 4-to-1 consolidation (12,000+ pcs) · Robot shells 30–50 sets (1/6 lead time). Source: GLUCK official portfolio (glucklab.com) · GLUCK technical blog (gluckblog.com/20, 102, 149) · Sculpia (sculpia.co.kr).
1. Executive Summary: Verified Before-and-After Transformation
Verified Metric: Tire master 120h to 30h (75% faster, ±0.06 mm) · Static mixer 4-to-1 consolidation (12,000+ pcs) · Robot shells 30–50 sets (1/6 lead time) (GLUCK official portfolio (glucklab.com) · GLUCK technical blog (gluckblog.com/20, 102, 149) · Sculpia (sculpia.co.kr)).
Rather than over-generalizing a single metric as a universal guarantee, this hub maps each verified case to its exact resin (G20-BR, G40-JG, White, Clear), bed envelope, finishing, and Creaform 3D scan gate.
When evaluating 20 Verified Before-and-After Industrial SLA & Sculpia Case Studies, what verified physical improvements did GLUCK's Paju 48-machine SLA smart factory achieve compared to traditional fabrication?
2. Legacy Process Bottleneck (Before) vs. Paju 48-Machine SLA Architecture (After)
Legacy Bottleneck (Before): 120-hour 5-axis CNC aluminum machining, 4-piece glued fluidic nozzles, high upfront tooling CapEx, and dusty hand-laid FRP delays.
GLUCK Single-Site SLA Solution (After): Single-site Paju 48-machine industrial SLA (600x600x400 mm standard and 1,000x800x600 mm monolithic beds) plus Sculpia digital archiving compressing lead times, part counts, and tooling CapEx.
| Comparison Dimension | Legacy Process (Before) | GLUCK Paju 48-SLA Process (After) | Verification Gate |
|---|---|---|---|
| Process & Tooling | 120-hour 5-axis CNC aluminum machining, 4-piece glued fluidic nozzles, high upfront tooling CapEx, and dusty hand-laid FRP delays | Single-site Paju 48-machine industrial SLA (600x600x400 mm standard and 1,000x800x600 mm monolithic beds) plus Sculpia digital archiving compressing lead times, part counts, and tooling CapEx | Single-site Paju 48-machine SLA |
| Measured Shift | Long tooling / machining queue | Tire master 120h to 30h (75% faster, ±0.06 mm) · Static mixer 4-to-1 consolidation (12,000+ pcs) · Robot shells 30–50 sets (1/6 lead time) | Creaform 3D laser scan & 6-Gate QA |
| Public Reference | Conventional vendor handoffs | GLUCK official portfolio (glucklab.com) · GLUCK technical blog (gluckblog.com/20, 102, 149) · Sculpia (sculpia.co.kr) | 1:1 engineer pre-order review |
Directory of 20 Verified Before-and-After Case Studies (#1301-#1320)
This flagship hub consolidates 12 industrial B2B engineering cases (#1301-#1312) and 8 contemporary art and Sculpia cases (#1313-#1320), strictly anchored to public GLUCK portfolio and blog documentation.
| Case | Project & Domain | Traditional Bottleneck (Before) | Verified Outcome (After) |
|---|---|---|---|
| #1302 | Hankook Precision Works Tire Mold Master Before-and-After Case | 5-axis CNC aluminum block machining requiring roughly 120 hours per tire master with heavy chip waste and micro-sipe cutter interference | Lead time 120h to 30h (75% reduction) · ±0.06 mm dimensional accuracy · Project-specific 95% process waste and 79% carbon reduction (gluckblog.com/20) |
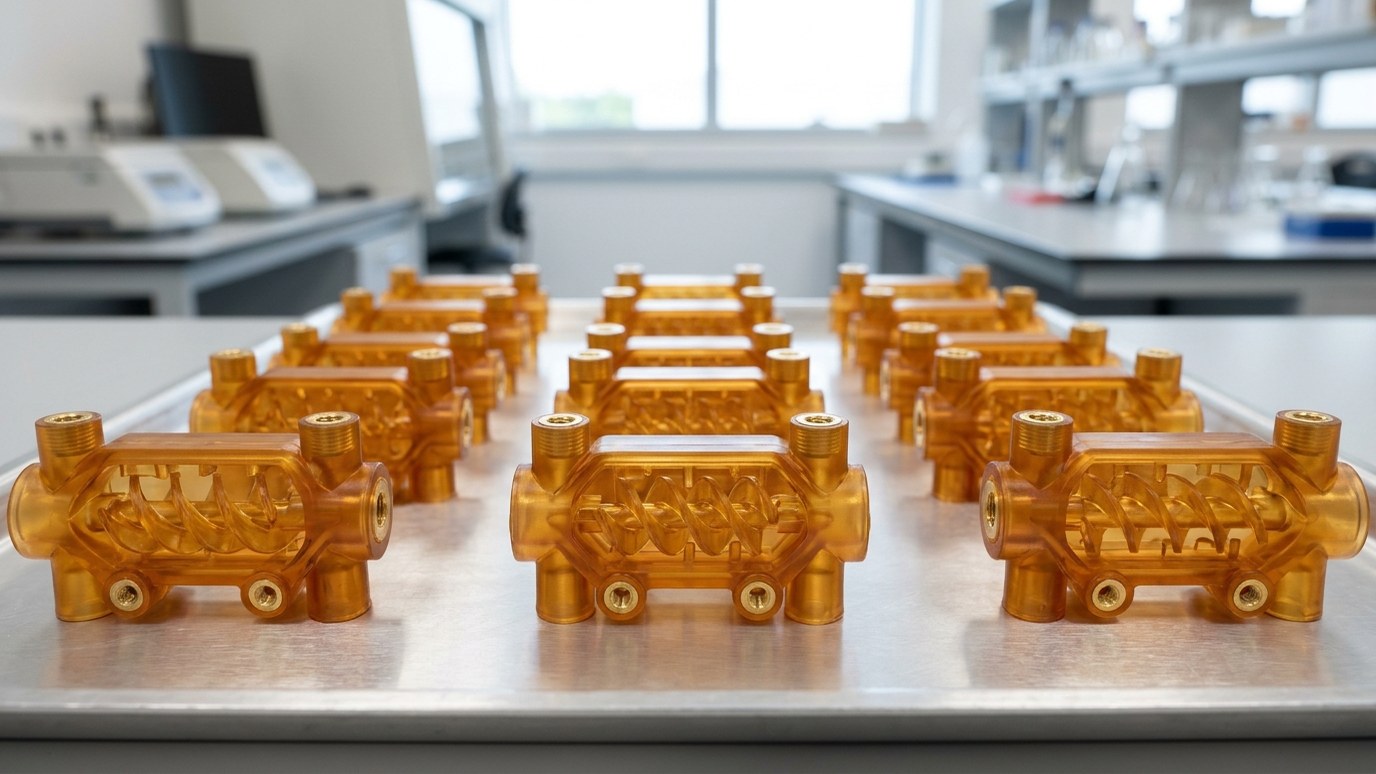
| #1303 | EV Battery Process Static Mixer Before-and-After Case | Assembling and bonding 4 separate molded/machined sub-components with seam leak risks and tolerance stack-up | 4 parts to 1 monolithic solid · Zero assembly steps · 12,000+ cumulative units delivered without tooling CapEx (idx=197) |
| #1304 | XYZ Service Robot 50-Set Exterior Shell Before-and-After Case | Conventional injection tooling for multi-panel curved robot exteriors required heavy upfront tooling CapEx and months of mold fabrication | 50 full robot exterior sets delivered without tooling · Development and initial production lead time compressed to roughly 1/6 of traditional tooling |
| #1305 | TWINNY Autonomous Mobile Robot (AMR) 30-Unit Exterior Before-and-After Case | Frequent LiDAR and depth-camera cutout revisions across a 30-unit AMR deployment outpaced silicone mold life (15-20 shots) and made hard tooling impractical | 30 AMR exterior sets delivered · Zero tooling rework cost across iterative sensor cutout ECOs |
| #1306 | Paju Smart Factory Robotic Sandblasting & Painting + Artisan Wet-Sanding Hybrid Post-Processing Case (gluckblog.com/149) | 100% manual blasting and base-coat spraying created operator fatigue bottlenecks and batch-to-batch surface variation on large lots | Robotic blasting/spray uniformity on batch runs + artisan wet-sanding & Zone B (0 μm paint) datum masking precision |
| #1307 | Civil & Industrial Drone 5-Full-Set 20-Day Delivery Before-and-After Case | Hand-laid carbon molds or hard tooling for UAV flight-test cowls required weeks of mold machining and blocked rapid sensor mount updates | 5 full industrial drone enclosure sets delivered within 20 days · Heat-set brass inserts and dust-sealing Step-Lip joints |
| #1308 | Aerospace Wind-Tunnel Aerodynamic Model Before-and-After Case | Machining, drilling, and brazing dozens of internal pressure-tap micro-channels inside metal wind-tunnel models demanded long lead times | Monolithic multi-channel pressure-tap routing · Wet-sanded airfoil skin with Creaform 3D laser scan deviation report |
| #1309 | Power-Tool & Industrial Device Housing Before-and-After Case | Standard prototyping resins (HDT 50-59°C) softened near motor heat or cracked when self-tapping screws were driven repeatedly | HDT 80°C thermal stability near motor mounts · M3-M6 heat-set brass inserts supporting repeated disassembly cycles |
| #1310 | Non-Implantable Medical Training Simulators Before-and-After Case | Slow manual assembly on training housings, layer-line transfer into silicone skin molds, and long lead times for anatomical vascular training models | 30-min assembly & 4-week faster development on gluteal simulator · Ra 0.8 μm mold finish · Strictly non-implantable training & display scope |
| #1311 | Mobility & Automotive R&D Dual Case Study | Thermal distortion on electric mobility drive housings and prohibitive stamping-die costs for >1,000 mm automotive fender and fascia R&D mockups | RDK & CO. G40-JG ±50 μm / Ra 0.8 μm / HDT 80°C · Large fender G20-BR split-bonding and automotive 2K PU finish |
| #1312 | High-Mix Low-Volume (HMLV) Digital Inventory Before-and-After Case | Storing aging molds or holding excess safety stock due to high injection-molding MOQs for intermittent equipment covers and jigs | Zero mold storage overhead · 6-month auto-purge for one-off RFQ CAD (immediate purge on NDA request) paired with locked P/N+Rev recipes for repeat bridge programs |
| #1313 | Sculptor's Clay Maquette Enlargement Before and After | Enlarging a 30 cm hand-sculpted clay maquette to two meters traditionally meant welding an armature, re-sculpting in clay, and laying plaster and fiberglass molds—filling the studio with dust and fumes while dulling delicate drapery folds. | Zero studio dust or fumes · True proportions carried from a 30 cm original to a 2 m centerpiece and 20 cm collector editions |
| #1314 | Yeesookyung x Namyang Shrine 'Our Lady Undoer of Knots' Story | Combining the quiet grace of the Pensive Bodhisattva and the Pieta with delicate hands untying a ribbon created deep veil hollows and thin ribbons that traditional molds struggled to release without damage. | Deep veil folds and delicate ribbon knots realized without mold seams · End-to-end collaboration from digital sculpting to sanctuary installation |
| #1315 | Frieze Seoul Park Seo-Bo Seated Portrait Statue Case | Recreating a late master's presence for an art-fair lounge by hand alone risked losing subtle facial likeness, while wax figures were vulnerable to warm exhibition lighting. | Lifelike skin creases, glasses, jacket weave and paint-spotted shoes · Stable museum-grade durability under lounge spotlights |
| #1316 | National Museum of Korea Baekje Gilt-Bronze Incense Burner 30th-Anniversary Miniature Case | With its perched phoenix, five tiny musicians, overlapping mountain peaks and dragon base, the Gilt-Bronze Incense Burner of Baekje was too intricate for conventional injection molds or ceramic slip-casting at miniature scale. | Intricate mountain filigree, phoenix and musician reliefs preserved at palm scale · Consistent quality across hundreds of collector pieces |
3. Scope Boundary, Resin Selection & Quality Assurance Gate
Rather than over-generalizing a single metric as a universal guarantee, this hub maps each verified case to its exact resin (G20-BR, G40-JG, White, Clear), bed envelope, finishing, and Creaform 3D scan gate. Standard online quoting supports up to 600x600x400 mm, while engineer-reviewed monolithic large beds cover up to 1,000x800x600 mm.
Request a 1:1 Engineer Custom 3D STEP Review ↗ · Open Interactive Bridge BEP Simulator ↗
Defense & Mobility Wind-Tunnel / Vibration Test Composite Spar (CFRP/GFRP), 360° Elastomeric Coating (173 MPa) & Helicoil Pull-Out Spec
Subsonic wind-tunnel aerodynamic models (30–65 m/s) for UAVs, eVTOLs, and defense mobility platforms require zero-deflection hybrid spars (AL6061 + CFRP/GFRP), shatter-containing 360° elastomeric polyurea coating (up to 173 MPa in 3-point flexural testing vs. 104 MPa uncoated), and stainless Helicoil inserts rated for 150–350 kgf axial pull-out loads.
| Defense & Wind-Tunnel Engineering Item | Target Test Specification | 5-Axis CNC Solid Machining / Unreinforced Resin | GLUCK Hybrid SLA + Composite Solution |
|---|---|---|---|
| Subsonic Wind-Tunnel Spar & Pressure Taps | Wingtip deflection ≤ 0.2mm at 30–65 m/s + monolithic 1.0–1.5mm internal pressure tap channels | 5-axis CNC cannot machine curved internal pressure routing (6–10 weeks, $30k–$70k); unreinforced resin deflects | High-modulus SLA outer skin (Ra 0.8μm finish) bonded to internal AL6061 spar + CFRP/GFRP composite layup (10–14 days, 45–60% cost reduction) |
| 1m Defense Louver 360° Elastomeric Coating | Up to 173 MPa 3-point flexural strength (vs. 104 MPa uncoated, coated coupon basis) with anti-spall containment | Uncoated brittle resin fractures into loose fragments under ballistic/vibration shock | 360° elastomeric polyurea encapsulation over heat-resistant SLA core captures internal fractures without spalling (undergoing vehicle mount validation) |
| Vibration Rig Helicoil Insert Pull-Out Load | M3–M8 stainless Helicoil / brass inserts · 150–350 kgf axial pull-out load per fastener · 50+ torque cycles | Direct plastic threads strip rapidly on multi-axis vibration shaker tables | Heat-set and structural-epoxy-locked stainless Helicoil and flanged nut inserts across all mounting bosses |
- Monolithic 30–80 Channel Internal Pressure Tap Routing: 1.0–1.5mm internal pneumatic channels are printed integrally inside airfoils and radomes, eliminating tube-gluing leaks.
- Air-Gapped Defense Security Protocol: Processed strictly on offline workstations at the Paju 48-machine SLA facility with 121-point optical calibration (±0.035–0.05mm) and automatic CAD purge after 6 months (or immediate permanent destruction upon NDA delivery).
Defense & Mobility Wind-Tunnel / Vibration Test Composite Spar (CFRP/GFRP), 360° Elastomeric Coating (173 MPa) & Helicoil Pull-Out Spec
Subsonic wind-tunnel aerodynamic models (30–65 m/s) for UAVs, eVTOLs, and defense mobility platforms require zero-deflection hybrid spars (AL6061 + CFRP/GFRP), shatter-containing 360° elastomeric polyurea coating (up to 173 MPa in 3-point flexural testing vs. 104 MPa uncoated), and stainless Helicoil inserts rated for 150–350 kgf axial pull-out loads.
| Defense & Wind-Tunnel Engineering Item | Target Test Specification | 5-Axis CNC Solid Machining / Unreinforced Resin | GLUCK Hybrid SLA + Composite Solution |
|---|---|---|---|
| Subsonic Wind-Tunnel Spar & Pressure Taps | Wingtip deflection ≤ 0.2mm at 30–65 m/s + monolithic 1.0–1.5mm internal pressure tap channels | 5-axis CNC cannot machine curved internal pressure routing (6–10 weeks, $30k–$70k); unreinforced resin deflects | High-modulus SLA outer skin (Ra 0.8μm finish) bonded to internal AL6061 spar + CFRP/GFRP composite layup (10–14 days, 45–60% cost reduction) |
| 1m Defense Louver 360° Elastomeric Coating | Up to 173 MPa 3-point flexural strength (vs. 104 MPa uncoated, coated coupon basis) with anti-spall containment | Uncoated brittle resin fractures into loose fragments under ballistic/vibration shock | 360° elastomeric polyurea encapsulation over heat-resistant SLA core captures internal fractures without spalling (undergoing vehicle mount validation) |
| Vibration Rig Helicoil Insert Pull-Out Load | M3–M8 stainless Helicoil / brass inserts · 150–350 kgf axial pull-out load per fastener · 50+ torque cycles | Direct plastic threads strip rapidly on multi-axis vibration shaker tables | Heat-set and structural-epoxy-locked stainless Helicoil and flanged nut inserts across all mounting bosses |
- Monolithic 30–80 Channel Internal Pressure Tap Routing: 1.0–1.5mm internal pneumatic channels are printed integrally inside airfoils and radomes, eliminating tube-gluing leaks.
- Air-Gapped Defense Security Protocol: Processed strictly on offline workstations at the Paju 48-machine SLA facility with 121-point optical calibration (±0.035–0.05mm) and automatic CAD purge after 6 months (or immediate permanent destruction upon NDA delivery).
Frequently Asked Engineering Questions
Is the 'Tire master 120h to 30h (75% faster, ±0.06 mm) · Static mixer 4-to-1 consolidation (12,000+ pcs) · Robot shells 30–50 sets (1/6 lead time)' outcome guaranteed universally across all geometries?
No. Rather than over-generalizing a single metric as a universal guarantee, this hub maps each verified case to its exact resin (G20-BR, G40-JG, White, Clear), bed envelope, finishing, and Creaform 3D scan gate. Every new 3D STEP drawing undergoes a 1-on-1 engineer review to confirm wall thickness, resin selection (G20-BR, G40-JG, White, Clear), and tolerance gates.
How does GLUCK verify dimensional accuracy before releasing a bridge lot?
First-article (1-5 unit) physical assembly fit-checks are combined with Creaform optical 3D laser scan colormap inspection and Zone B (0 um paint) datum masking.
How are 3D CAD files governed after prototype or bridge delivery?
One-off RFQ CAD files are retained on the isolated Paju network for 6 months and then automatically purged (with immediate deletion available upon NDA request), while repeat bridge items are locked under P/N + Revision.
What are the CFRP/GFRP composite spar, 173 MPa elastomeric coating, and Helicoil insert pull-out specifications for defense wind-tunnel and vibration test models?
To keep wingtip deflection under 0.2mm at 30–65 m/s subsonic wind-tunnel loads, we combine an Ra 0.8μm SLA aerodynamic shell with an internal AL6061 spar and CFRP/GFRP composite layup, apply a 360° elastomeric polyurea coating achieving up to 173 MPa in 3-point flexural testing (versus 104 MPa uncoated, with anti-spall fragment containment), and lock M3–M8 stainless Helicoil inserts rated for 150–350 kgf axial pull-out load.
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
Evaluates schedule compression, part consolidation, and mold-CapEx avoidance when transitioning legacy CNC master patterns, multi-piece glued manifolds, or hand-laid FRP shells onto GLUCK's single-site 48-machine Paju industrial SLA line (600×600×400 mm standard and up to 1,000×800×600 mm monolithic beds) gated by 1–5 first-article verification.
- Case-Specific Benchmark Attribution: Published lead-time and waste-reduction metrics (such as tire master patterns, 4-to-1 static mixers, and robot cowls) reflect their specific verified geometries; new programs receive a 1:1 engineer DFM quote
- Mandatory 1–5 Unit First-Article Fit-Check Before 100+ Unit Parallel Bridge Releases
- Creaform 3D Laser Scan Colormap Inspection & Locked P/N+Rev Process Recipes for Repeat Lots
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |