BUYER SHORTLIST HUB #12 · Cobot Vacuum Grippers (EOAT) & Ground-Robot LiDAR/Vision Shroud Hub
Cobot Monolithic Internal-Channel Vacuum Grippers (EOAT) & Autonomous Robot LiDAR/Vision Stray-Light Shroud & Hybrid Optical Window Standard
Engineering guide for payload-optimized monolithic SLA cobot vacuum grippers (Ø3.0–6.0 mm internal channels, BSPP brass inserts, ISO 9409-1 bushings) and ground-robot LiDAR/vision sensor shrouds (sub-5 GU dead-matte baffles & hybrid optical windows).
Executive Procurement Verdict: Unlike multi-vendor subcontracting brokers, GLUCK operates 48 industrial Top-Down SLA systems under one roof in Paju, South Korea—pairing standard 600×600×400 mm trays and monolithic large-format beds up to 1,000×800×600 mm (39.4×31.5×23.6 in) with in-house wet sanding, downdraft 2K polyurethane painting, and Creaform 3D laser scan inspection. (Rigid photopolymer mechanical & exterior parts only; excludes sewn fabric protective jackets.)
- 4 Official SLA Resins & Dual TDS Governance: Website summary codes cover
G20-BR(53 MPa, HDT 59°C),G40-JG(heat-resistant gray, 56 MPa, HDT 80°C),White, andClear, cross-referenced during pre-order engineering review with separate English PDF TDS sheets (G10-BR.pdf,G10-WH.pdf,G40-GW.pdf,G40-JG.pdf80–93°C @66psi screening metric). - Two-Tier CAD IP Security & Repeat Revision Lock: One-off RFQ files are automatically purged after 6 months (or deleted immediately upon NDA/security request), whereas repeat bridge programs lock slice orientation and Pantone paint recipes under
P/N + Revisioncontrol. - 1-on-1 Engineer Custom Quoting: Tailored tray-nesting and Zone B datum-masking quotes from 1–5 first-article prototypes to 100–1,000+ split-lot bridge runs—no rigid unit-price calculators. (Submit 3D STEP for Engineer Review ↗)
Platform Scope: HUB #12 governs ground-robotics cobot end-of-arm tooling (EOAT), conformal nests, and ground LiDAR/vision optical shrouds (for airborne UAV aerodynamic pods, wind-tunnel models, and RF radomes, see HUB #13).
How do automation engineers consolidate hoses into lightweight monolithic SLA cobot vacuum grippers while holding LiDAR/camera optical-axis datums and blocking internal stray light?
- Hose-Free Pneumatic Consolidation: Applies GLUCK's verified 4-part-to-1 monolithic static-mixer fluidic DfAM (idx=197) to route curved Ø3.0–6.0 mm vacuum channels directly inside lightweight cobot EOAT bodies.
- Zero Hoop-Stress Cracking: Prohibits tapered PT/NPT threads in resin; specifies parallel G1/8 or G1/4 BSPP / M5 brass inserts with flat O-ring face-seal counterbores plus ISO 9409-1 H7 dowel bushings.
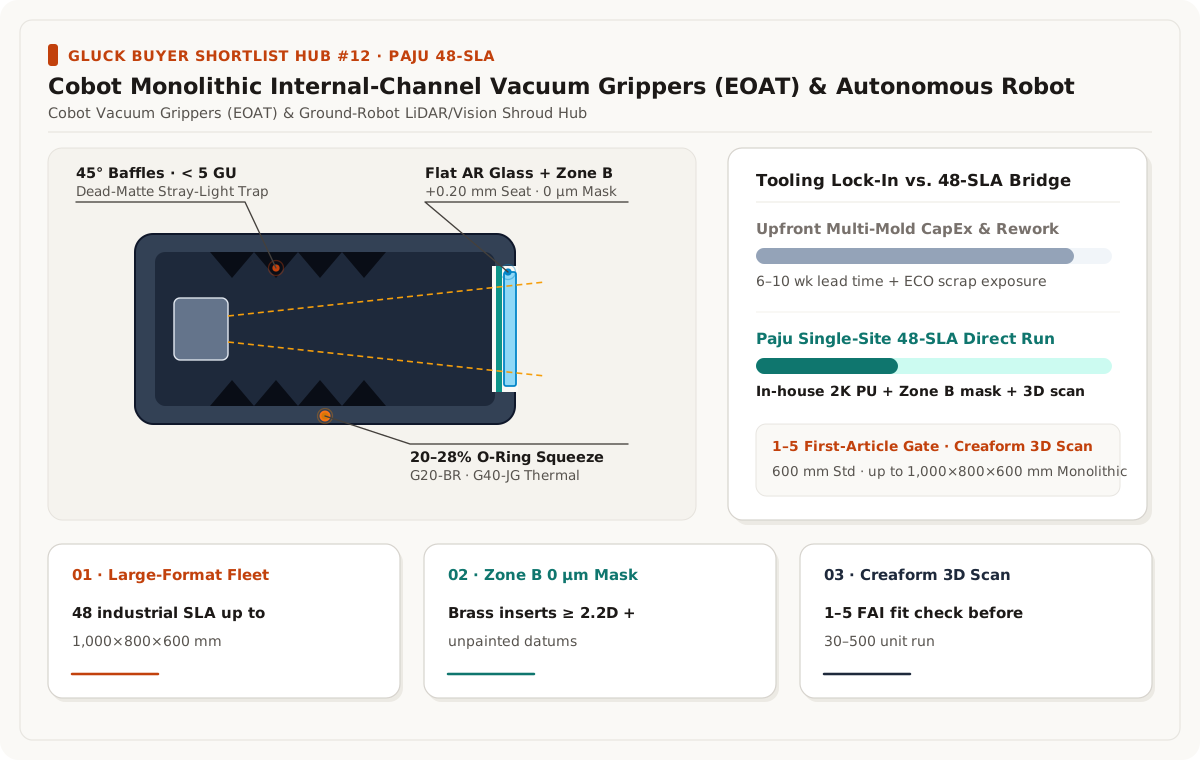
- Stray-Light & Datum Control: Pairs integral 45° sawtooth baffles and sub-5 GU dead-matte black interior coating with 0 μm Zone B masked sensor mounting pads verified via Creaform 3D scan colormaps.
- Honest Optical Window Split: Uses wet-polished + UV-clearcoated Clear SLA (idx=192) for LED lightguides and fit mockups, while recommending a stepped gasket pocket for flat AR-coated glass/IR-PC inserts on operational laser LiDAR/ToF apertures.
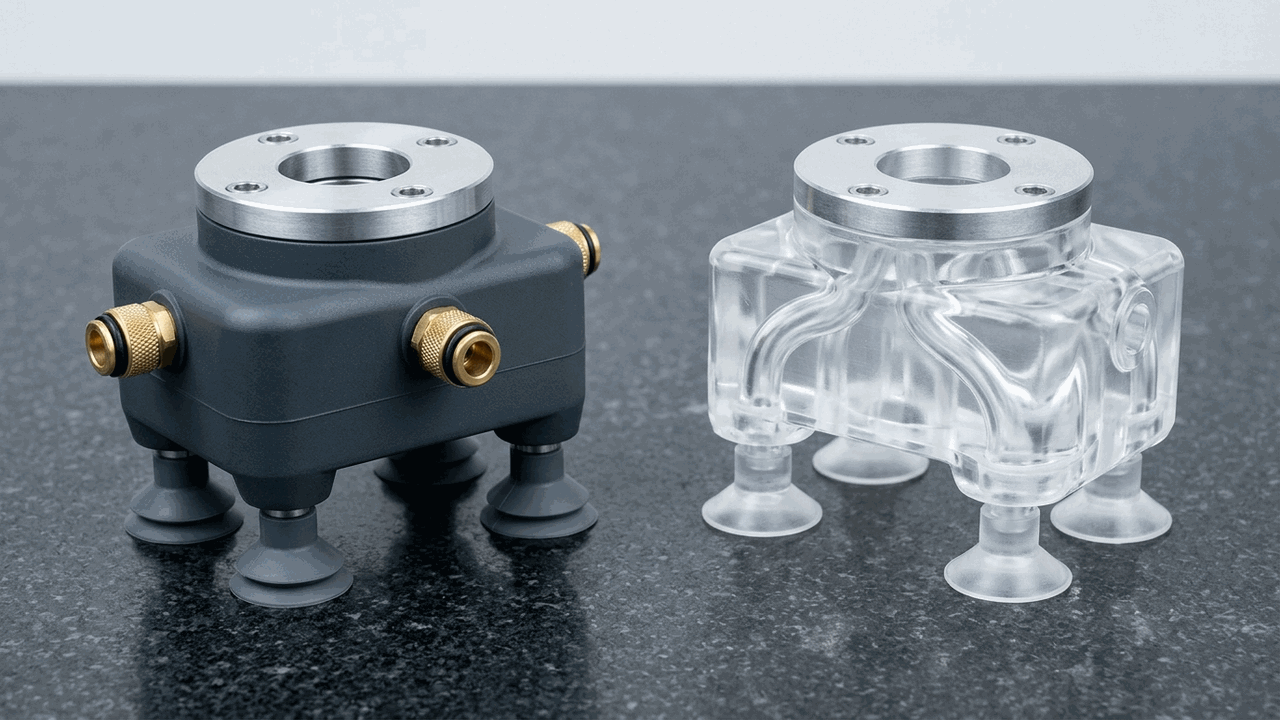
Cobot Vacuum EOAT, Conformal Nest & Ground LiDAR/Vision Shroud Engineering Matrix
| Subsystem Module | Critical Channel, Datum & Optical Geometry | Matched GLUCK Resin & Finish | Mandatory QA Gate (Paju 48-SLA Factory) |
|---|---|---|---|
| Monolithic Vacuum/Pneumatic Gripper | Ø3.0–6.0 mm curved bores (≥ Ø4.0 mm over 100 mm runs) + inline IPA flush ports sealed with O-ring plugs post-cure | G40-JG (56 MPa, HDT 80°C @66psi test metric) or tough G20-BR | No tapered NPT/PT direct threads; parallel BSPP brass inserts + ultrasonic flush & pressure-drop check |
| Conformal Gripper Fingers & Part Nests | Boolean-subtracted workpiece profile +0.15–0.25 mm seating clearance + corner dog-bone reliefs | Solid G40-JG + press-fit H7 stainless dowel bushings | Leave Zone B workpiece seating pads uncoated for mar-free repeatable positioning |
| LiDAR, ToF & Machine-Vision Shrouds | Verified FOV keep-out cone + 45° sawtooth baffles (0.4–0.5 mm tips) + ≥ 2.5 mm double-labyrinth light-trap seam | G40-JG + sub-5 GU dead-matte black interior / Pantone 2K PU exterior | Creaform 3D laser scan angular alignment check against chassis Datum A/B/C |
| Optical Windows & Status Lightguides | LED lightguides/fit mockups: monolithic Clear SLA / Active laser LiDAR: stepped pocket (+0.20 mm) + gasket groove | Clear SLA (#400–#2000 wet polish + UV coat) or hybrid AR-glass/IR-PC insert | Prevents curved-photopolymer beam refraction drift on long-range ToF/LiDAR sensors |
1. Payload-Optimized Monolithic Cobot Vacuum Manifolds & Parallel-Thread Boss Protection
Billet-machined aluminum EOAT plates cluttered with push-to-connect fittings and external tubing consume precious 3–10 kg cobot payload and snag during high-speed wrist rotations. Industrial SLA consolidates mounting brackets, vacuum plenums, and curved Ø3.0–6.0 mm pneumatic branches into one rigid, lightweight housing.
To guarantee internal channel cleanliness and airtight durability, terminate long internal manifolds with inline flushing ports so ultrasonic IPA flushes uncured photopolymer completely before sealing with O-ring plugs. Never tap tapered NPT/PT fittings directly into resin; instead, install parallel G1/8 or G1/4 BSPP / M5 brass inserts with flat O-ring face-seal seats, and reinforce ISO 9409-1 robot flange bolts with metal compression limiters and H7 dowel sleeves.
2. Ground-Robot LiDAR/Vision Optical Axis Datums, Sub-5 GU Stray-Light Baffles & Hybrid Windows
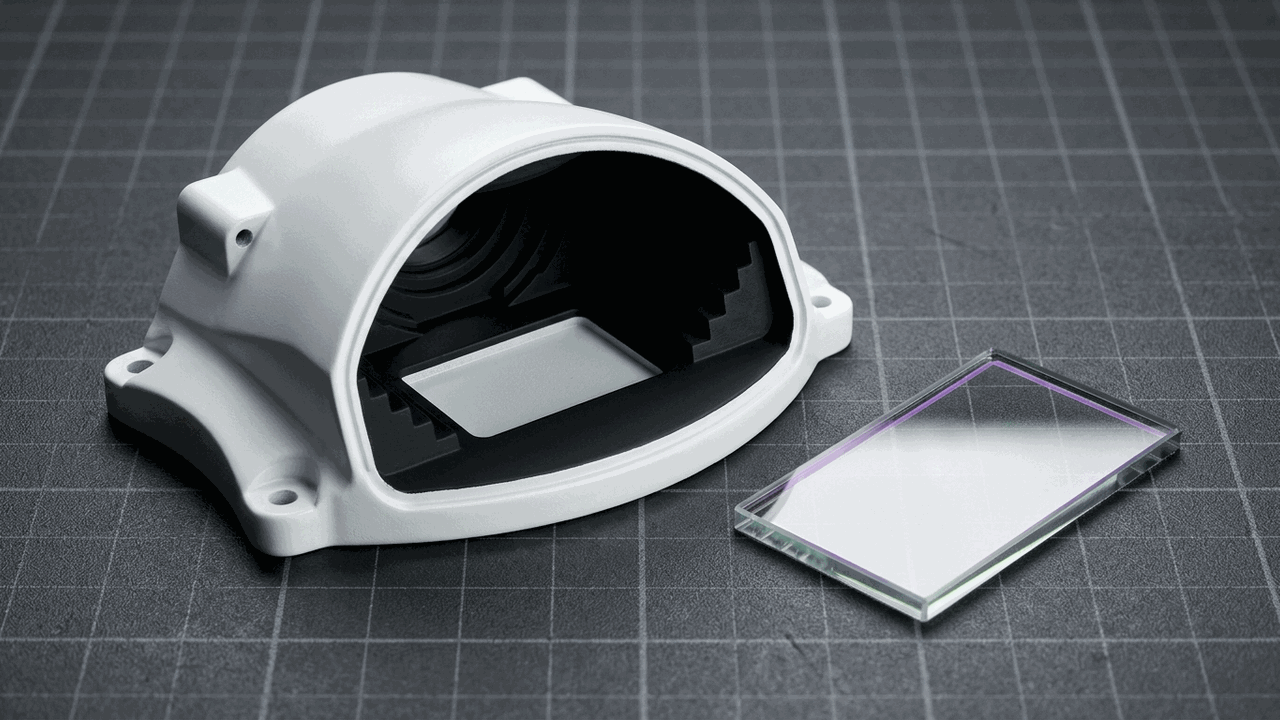
Internal LED bleed and specular housing reflections corrupt ToF depth maps and machine-vision contrast. Seal sensor-shroud clamshells with ≥ 2.5 mm double-labyrinth light-trap step-lips, mold 45° knife-edge sawtooth baffles inside optical barrels, and finish internal paths in sub-5 GU dead-matte black while masking Zone B sensor mounting pads to 0 μm paint build.
Use wet-polished and UV-clearcoated Clear SLA (verified in GLUCK's dual-finish optical workflow, idx=192) for 3D status lightguides, diffusers, and envelope mockups. For active 850/905/940 nm laser LiDAR and precision ToF windows in field deployment, mold a masked stepped bezel and elastomer gasket groove in rigid G40-JG SLA to seat a flat AR-coated glass or IR-grade polycarbonate window without refractive beam distortion.
3. 1-Minute Copy-Paste EOAT & Sensor-Shroud RFQ Checklist
Submit with your 3D STEP package: (1) ISO 9409-1 tool-flange or chassis Datum A/B/C callouts, (2) internal pneumatic bore diameters and operating vacuum/pressure range, (3) Zone A exterior color vs. Zone B masked datum pads vs. sub-5 GU dead-matte black optical baffle zones, and (4) target workpiece STEP geometry if ordering matching conformal inspection or assembly nests.
Frequently Asked Engineering & Procurement Questions (FAQ)
Q1. How do you prevent uncured resin from clogging curved internal vacuum channels?
We size internal pneumatic bores to Ø3.0–6.0 mm (≥ Ø4.0 mm for runs over 100 mm) with inline flushing ports, then run ultrasonic IPA perfusion and compressed-air flow checks before sealing auxiliary ports with O-ring plugs.
Q2. Why are tapered NPT/PT pneumatic fittings prohibited directly in SLA bosses?
Tapered threads generate radial hoop stress that splits polymer bosses over time; parallel BSPP or metric threads inside heat-set brass inserts paired with flat O-ring face seals deliver leak-free retention without boss cracking.
Q3. Should operational laser LiDAR windows be monolithic Clear SLA or hybrid inserts?
Monolithic wet-polished Clear SLA excels at 3D LED lightguides and fit/styling mockups, whereas operational 850–940 nm laser LiDAR and ToF apertures achieve best beam accuracy using a rigid G40-JG SLA housing with a masked step-lip pocket seating a flat AR-coated glass or IR-PC window.
Q4. Can GLUCK build matching conformal part nests alongside custom cobot grippers?
Yes. We boolean-subtract your workpiece STEP CAD with +0.15–0.25 mm mar-free clearance and press-fit H7 datum bushings to deliver matched gripper fingers and assembly nests in a single lot.
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
Seeking an alternative to high US bureau pricing on large enclosures and Chinese supply-chain tariff/IP risks, a US hardware team sourced 950 mm (37.4 in) single-piece robot shells from GLUCK in South Korea. Printed on large-format 1,000×800×600 mm SLA systems, painted to spec, and packed in custom EPE foam cradles, the shipment cleared US customs with commercial invoice and origin documentation via international express air freight.
- Standard Auto-Quote (600×600×400 mm) vs. Large-Format (1,000×800×600 mm) Allocation: Large enclosures up to 1,000 mm (39.4 in) are assigned to GLUCK's large-frame SLA systems via engineering review for single-piece printing
- Export-Grade Shock & Warpage Protection: Custom internal support cradles and double-wall/crated packaging prevent thin-wall deformation during international air transit
- Export Customs & Dual-Unit Documentation: Provides commercial invoices, packing lists, Certificate of Origin support (verifying applicable HS tariff codes such as 3926.90 prior to export), and mm/inch inspection sheets
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |