EO/IR Gimbal Housings, Rotational-Inertia (J) Isogrid LightWeighting & Honest G40-JG Thermal Boundaries: Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque (174 mm / 6.9 in) Moldless SLA Bridge Production, TCO & CAD-MCP STEP Flagship Guide
Physical DfAM Wall/Rib/Slot Sizing & Honest Resin Thermal-Mechanical Boundary for Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque (174 mm / 6.9 in). Paju 48-SLA playbook pairing G40-JG, Zone B 0 μm masking, and Creaform 3D scan FAI across 40-set runs.
1. Buyer & Lead-Engineer Specification Briefing
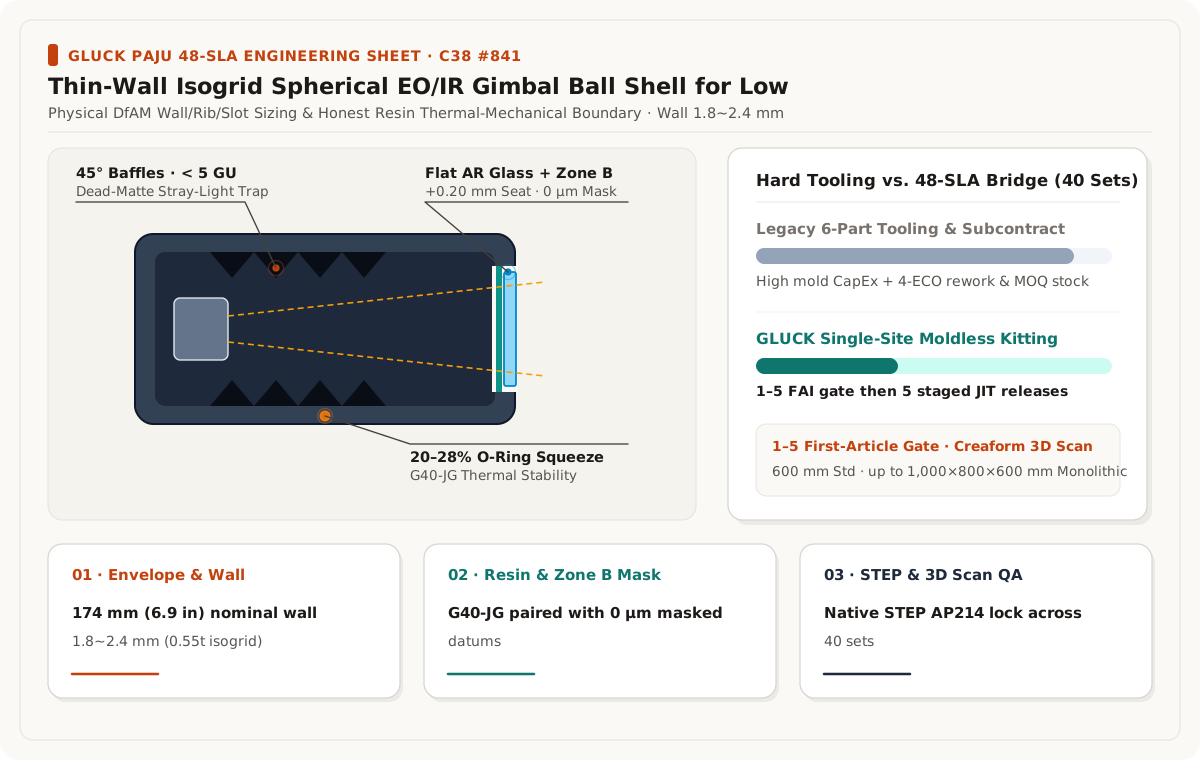
On service-cycled assemblies like a Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque (6.9 in / 174 mm), coating buildup and boss hoop stress drive most early failures. Enforcing hemisphere split step-lips and optical barrel rims masked to Zone B 0 μm + sub-5 GU internal baffle paint alongside G40-JG (~2,700 MPa flexural modulus with 0.1 g digital-scale mass logging across every printed hemisphere) locks tolerances on the very first build.
Scope Boundary: Lightweight EO/IR gimbal balls, yokes, and optical bezels for UAVs and robotics (core heatsinks above 80–120 °C isolate onto aluminum subframes; photopolymer Clear resin is opaque to LWIR thermal bands).
2. Structural DfAM Dimensions for Vibration, Fastening & Field Service
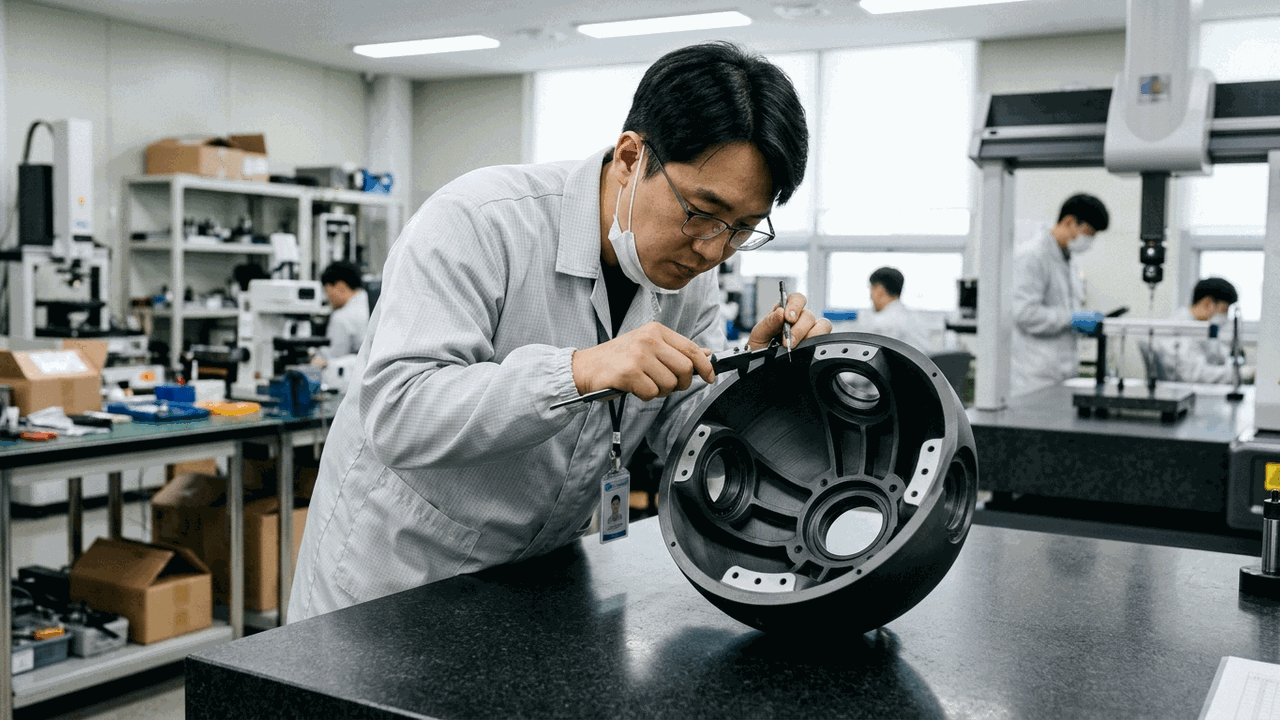
Every gram trimmed from outer-radius EO/IR gimbal hemispheres lowers BLDC stabilization torque. Thin 1.8–2.4 mm G40-JG skins stiffened by CG-balanced 0.55t triangular isogrid ribs undergo 0.1 g digital mass logging on every part.
Engineering drawings specify nominal 1.8~2.4 mm (0.55t isogrid) wall sections alongside hemisphere split step-lips and optical barrel rims masked to Zone B 0 μm + sub-5 GU internal baffle paint so Class-A coating never compromises mechanical seating.
| Control Dimension | Quantitative Target & Scenario | Resin & Process Governance | Verification Gate |
|---|---|---|---|
| Module & Span (#841) | Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque / 174 mm (6.9 in) · Wall 1.8~2.4 mm (0.55t isogrid) | 600×600×400 mm standard bed 48-SLA parallel kit nesting | 1–5 set physical bolt-pitch fit check |
| DfAM & Resin Rule (G40-JG) | triangular internal isogrid ribs minimizing rotational inertia (J = ∫r²ρdV) + CG-balanced rib density | G40-JG (~2,700 MPa flexural modulus with 0.1 g digital-scale mass logging across every printed hemisphere) | Pre-build load & thermal boundary review |
| Zone A/B/C Datum Control | Zone A 2K PU finish / Zone B 0 μm masked mating datums | hemisphere split step-lips and optical barrel rims masked to Zone B 0 μm + sub-5 GU internal baffle paint | 3-2-1 datum Creaform 3D scan audit |
| Bridge & Digital Thread | Illustrative 40 sets (6-part kit · 5 lots · 4 Revs) | Rhino 8 wall-thickness map & Fusion 360 interference check on native STEP (AP214) | STEP SHA-256 lock + Zone C deboss |
3. Parametric CAD Automation & Optical 3D Scan Closed-Loop Metrology
During pre-flight DFM review, Rhino 8 wall-thickness map & Fusion 360 interference check on native STEP (AP214) audits nominal wall sections (1.8~2.4 mm (0.55t isogrid)) and IPA drain paths. Post-cured first articles are inspected on a granite surface plate via optical 3D scanning before entering the 2K PU spray booth.
4. Pre-Tooling Design De-Risking Economics & RFQ Intake Protocol
On a 6-part Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque shipset, bundled multi-mold CapEx across 6 tools and 4 expected design revisions dominates unit piece price. Evaluating total kit TCO across an illustrative 40-set bridge program favors freezing tolerances on 1–5 physical SLA units before parallel 48-machine toolless kitting.
3-Track Engineer RFQ Routing for Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque (174 mm)
[Track A STEP Bridge] STEP (AP214) + Zone A/B/C notes + 40-set/5-lot cadence · [Track B Mutual NDA] Pre-RFQ NDA + shell-only intake + immediate post-delivery CAD purge · [Track C EOL Scan / AI Mesh] Creaform 3D scan or B-Rep STEP rebuild gated by 1-unit fit check.
Engineering & Bridge Sourcing FAQ
[#841] Why choose 48-SLA bridge production over hard tooling for 40 sets of a Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque (174 mm)?
Across a 6-part shipset, moldless SLA avoids upfront multi-cavity tooling CapEx, absorbs 4 field-test ECO revisions with zero scrap, and ships across 5 JIT lots.
How does GLUCK hold assembly tolerances around triangular internal isogrid ribs minimizing?
By pairing nominal 1.8~2.4 mm (0.55t isogrid) wall sections with hemisphere split step-lips and optical barrel rims masked to Zone B 0 μm + sub-5 GU internal baffle paint, isolating 40–60 μm cosmetic 2K PU paint films from 0 μm masked functional datums.
What material and CAD checks apply to G40-JG using Rhino 8 wall-thickness map?
Designs respect G40-JG (~2,700 MPa flexural modulus with 0.1 g digital-scale mass logging across every printed hemisphere) boundaries and submit watertight B-Rep STEP (AP214) geometry gated by a 1–5 unit physical fit check and Creaform 3D laser scan audit.
What RFQ details accelerate custom engineer quoting for 40 sets of a Thin-Wall Isogrid Spherical EO/IR Gimbal Ball Shell for Low Stabilization-Motor Torque?
Provide STEP (AP214) files, Zone A Pantone/RAL & gloss GU, Zone B 0 μm masked datums, target 40-set / 5-lot schedule, and Creaform 3D scan FAIR scope.
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
To reduce rotational inertia on a 3-axis stabilized gimbal ball, internal triangular isogrid ribs stiffen a thin G40-JG shell (homepage summary HDT 80 °C; English TDS 80–93 °C @ 66 psi screening metric) across a 35-set batch. Bearing bores use +0.02–0.04 mm slip-fit shaft-aligned bonding rather than press-fitting to prevent hoop-stress creep.
- Honest 4-Zone Thermal Boundary: Treats G40-JG HDT as a screening metric—applying ≥5–10 mm air gaps and thermal-soak trials for 55–75 °C electronics while isolating above 80–120 °C core heatsinks on aluminum subframes
- Slip-Fit Bearing Bonding & Flat Optical Window Seats: Eliminates press-fit hoop cracking and masks flat Germanium/AR-glass seats (noting photopolymer Clear resin does not transmit LWIR)
- Gram-Level Digital Scale Mass Logging & Creaform 3D Scan Coaxiality Check Across Gimbal Yoke Bores
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |