Humanoid Torso & Limb Shells, Pinch-Guard Clearances & Impact-Rib Bridge Production: 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell (820 mm / 32.3 in) Moldless SLA Bridge Production, TCO & CAD-MCP STEP Flagship Guide
Physical DfAM Wall/Rib/Slot Sizing & Honest Resin Thermal-Mechanical Boundary for 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell (820 mm / 32.3 in). Paju 48-SLA playbook pairing G20-BR, Zone B 0 μm masking, and Creaform 3D scan FAI across 40-set runs.
1. Executive Engineering Summary & Scope Boundary
When aligning mechanical design and bridge procurement on an 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell (820 mm / 32.3 in), field reliability hinges on internal 0.55t tapered honeycomb impact ribs (R 1.5 mm root fillet) and EPDM grommet floating mounts. GLUCK's 48-machine Paju SLA fleet pairs G20-BR (toughness-screened ABS-like SLA, HDT 59 °C · 1,000×800×600 mm monolithic build) with 1–5 unit first-article checks before scaling 40-set deliveries.
Scope Boundary: Rigid photopolymer SLA exterior shells and painted joint shrouds for humanoid and bipedal robots (excludes sewn fabric protective jackets and metallic harmonic-drive gears).
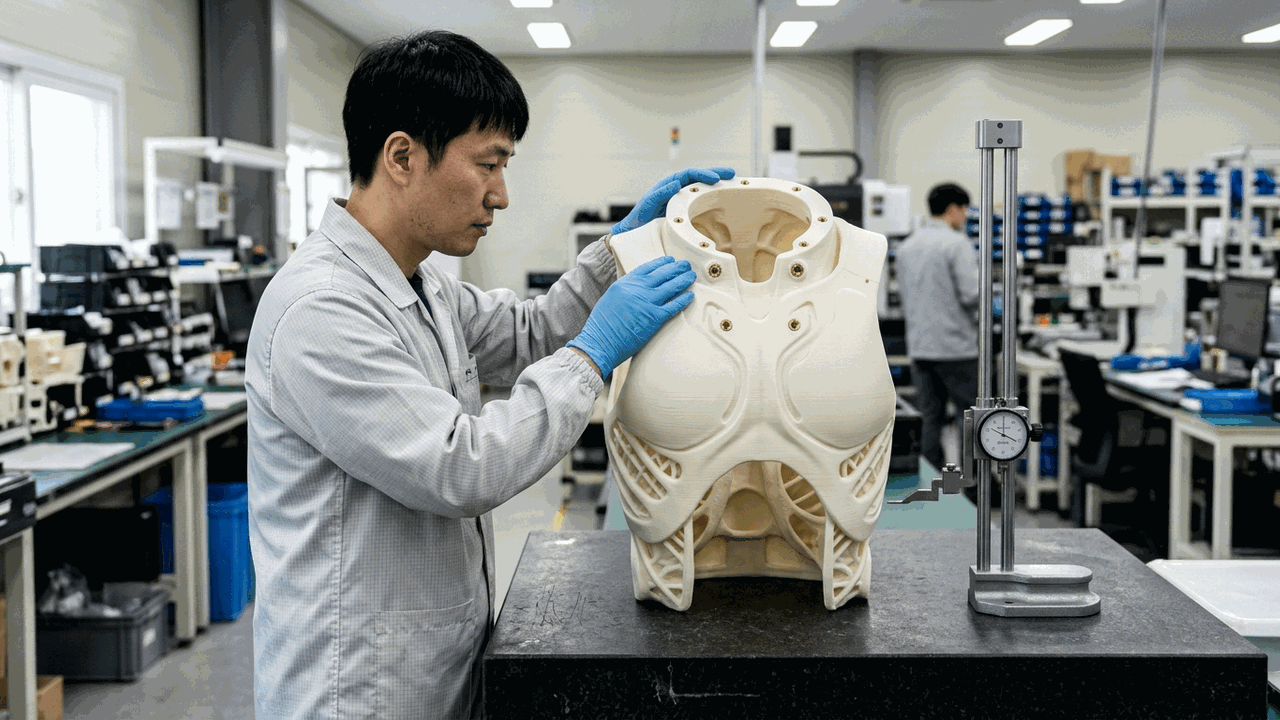
2. Subsystem Physical DfAM Rules & Zone A/B/C Masking Isolation
The main humanoid chest and dorsal torso shell absorbs peak ground-impact momentum during gait-trial falls. Tapered 0.55t honeycomb internal ribs spread impact energy without exterior paint sink marks, while six spine-frame mounts isolate bolt preload through EPDM grommets and steel sleeves.
Engineering drawings specify nominal 3.2~3.8 mm wall sections alongside 6 aluminum spine-frame seating pads masked to Zone B 0 μm + heat-set brass inserts (boss OD ≥ 2.2D) so Class-A coating never compromises mechanical seating.
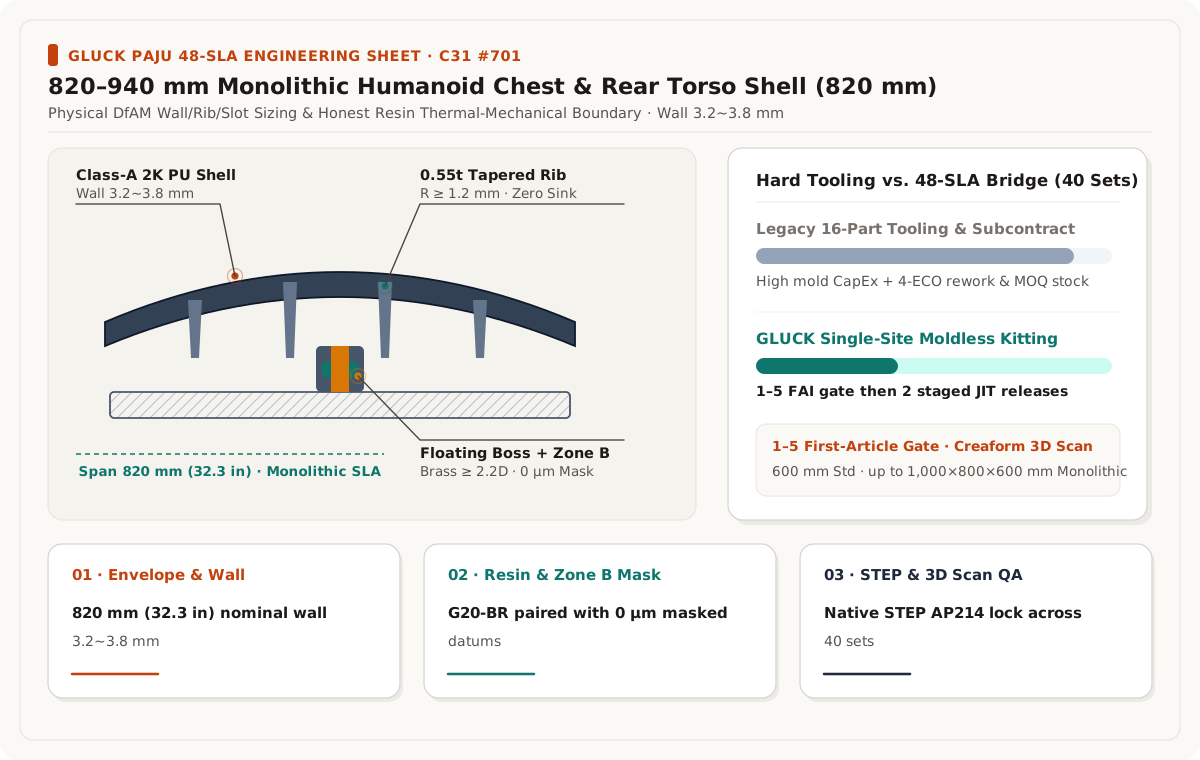
3. Moldless Bridge Production Economics & 48-SLA Parallel Kitting
On a 16-part 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell shipset, bundled multi-mold CapEx across 16 tools and 4 expected design revisions dominates unit piece price. Evaluating total kit TCO across an illustrative 40-set bridge program favors freezing tolerances on 1–5 physical SLA units before parallel 48-machine toolless kitting.
| Control Dimension | Quantitative Target & Scenario | Resin & Process Governance | Verification Gate |
|---|---|---|---|
| Module & Span (#701) | 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell / 820 mm (32.3 in) · Wall 3.2~3.8 mm | 1,000×800×600 mm large-format monolithic bed via engineer allocation | 1–5 set physical bolt-pitch fit check |
| DfAM & Resin Rule (G20-BR) | internal 0.55t tapered honeycomb impact ribs (R 1.5 mm root fillet) and EPDM grommet floating mounts | G20-BR (toughness-screened ABS-like SLA, HDT 59 °C · 1,000×800×600 mm monolithic build) | Pre-build load & thermal boundary review |
| Zone A/B/C Datum Control | Zone A 2K PU finish / Zone B 0 μm masked mating datums | 6 aluminum spine-frame seating pads masked to Zone B 0 μm + heat-set brass inserts (boss OD ≥ 2.2D) | 3-2-1 datum Creaform 3D scan audit |
| Bridge & Digital Thread | Illustrative 40 sets (16-part kit · 2 lots · 4 Revs) | Rhino 8 wall-thickness map & Fusion 360 interference check on native STEP (AP214) | STEP SHA-256 lock + Zone C deboss |
4. AI 3D / CAD-MCP B-Rep STEP Pipeline & Creaform 3D Scan FAI Loop
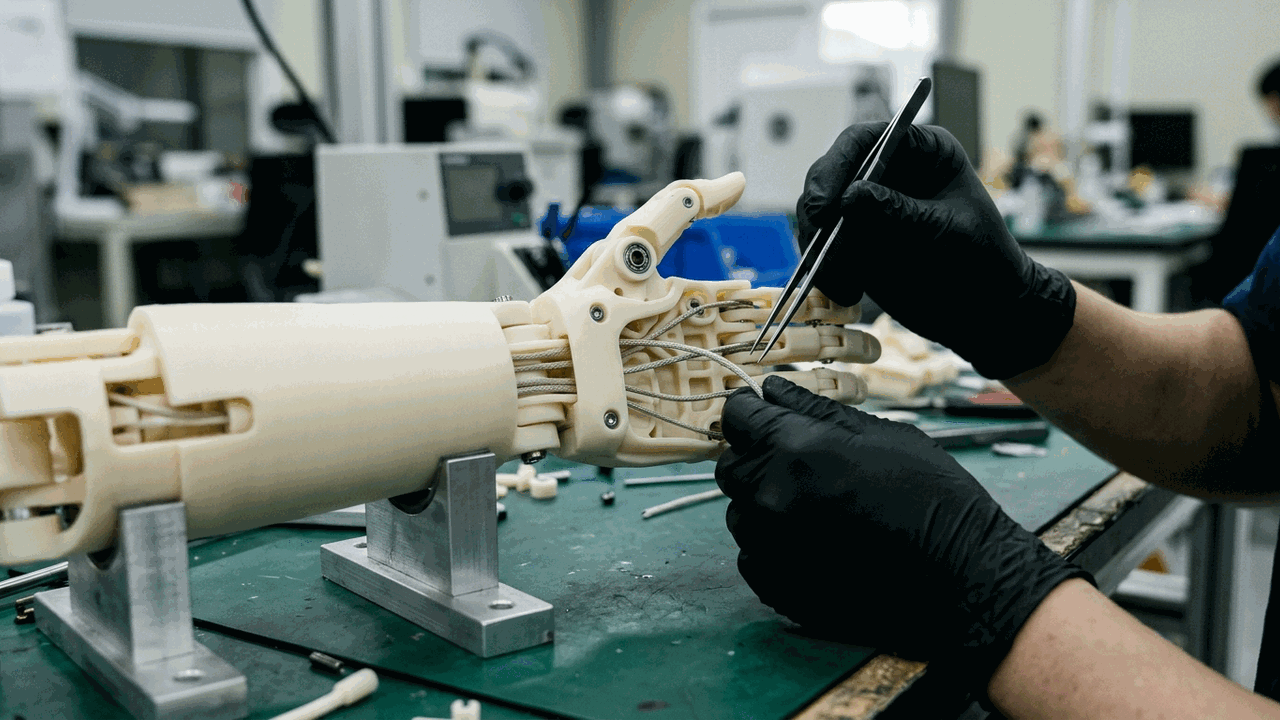
Pre-build geometry preparation runs Rhino 8 wall-thickness map & Fusion 360 interference check on native STEP (AP214) to eliminate non-manifold edges and out-of-round boss tessellation. Engineers then test-fit 1–5 printed first articles on live hardware and verify 3-2-1 datum deviations via Creaform optical 3D scan color maps before releasing 40 sets.
3-Track Engineer RFQ Routing for 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell (820 mm)
[Track A STEP Bridge] STEP (AP214) + Zone A/B/C notes + 40-set/2-lot cadence · [Track B Mutual NDA] Pre-RFQ NDA + shell-only intake + immediate post-delivery CAD purge · [Track C EOL Scan / AI Mesh] Creaform 3D scan or B-Rep STEP rebuild gated by 1-unit fit check.
Engineering & Bridge Sourcing FAQ
[#701] Why choose 48-SLA bridge production over hard tooling for 40 sets of an 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell (820 mm)?
Across a 16-part shipset, moldless SLA avoids upfront multi-cavity tooling CapEx, absorbs 4 field-test ECO revisions with zero scrap, and ships across 2 JIT lots.
How does GLUCK hold assembly tolerances around internal 0.55t tapered honeycomb impact ribs?
By pairing nominal 3.2~3.8 mm wall sections with 6 aluminum spine-frame seating pads masked to Zone B 0 μm + heat-set brass inserts (boss OD ≥ 2.2D), isolating 40–60 μm cosmetic 2K PU paint films from 0 μm masked functional datums.
How are 820 mm (32.3 in) spans built when they exceed the 600×600×400 mm web instant-quote default?
Engineer batch review allocates parts up to 1,000×800×600 mm onto large-format monolithic SLA beds unsplit; spans above 1,000 mm use 0.20 mm epoxy-gap step-lips backed by internal metal straps.
What RFQ details accelerate custom engineer quoting for 40 sets of an 820–940 mm Monolithic Humanoid Chest & Rear Torso Shell?
Provide STEP (AP214) files, Zone A Pantone/RAL & gloss GU, Zone B 0 μm masked datums, target 40-set / 2-lot schedule, and Creaform 3D scan FAIR scope.
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
To produce 60 sets of 16 asymmetric freeform humanoid torso and limb covers without upfront injection-mold CapEx, an engineering review pairs GLUCK's 48-machine Paju SLA fleet with its 1,000×800×600 mm large-format envelope. Internal 0.55t tapered impact ribs, EPDM vibration grommets with metal compression limiters, and zero-tooling Rev.A-to-Rev.B joint-clearance updates de-risk the 60-unit deployment fleet.
- Sink-Free Internal Impact Ribbing: Keeps rib thickness at 0.55x outer wall (t=3.0–3.8 mm) with R ≥ 1.2 mm root fillets to absorb fall energy without Class-A read-through
- URDF Swept-Envelope Pinch Clearance: Verifies +4.0–6.0 mm dynamic joint clearance and Zone B 0 μm masking on frame seating pads
- First-Article Full-Skeleton Fit-Check & Creaform 3D Scan: Validates left/right symmetry before parallel per-robot kit printing
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |