First-Release Cash Outflow Comparison: Upfront Mold + Full MOQ Outlay vs. Paying Only for Release #1 Demand (d[1])
First-Release Cash Outflow Comparison — Direct Engineering Standard: In First-Release Cash Outflow Comparison: Upfront Mold + Full MOQ Outlay vs. Paying Only for Release #1 Demand (d[1]), procurement and engineering teams compare total injection molding cost CM(Q) = FM + Q·pM against moldless industrial SLA cost CA(Q) = FA + Q·pA to locate the true break-even volume N* = ceil((FM - FA)/(pA - pM)). As validated in Warehouse AGV Manufacturer · 600 Annual Units Delivered in 4 Quarterly Batches of 150, Although annual demand totaled 600 AGV sensor covers, the assembly line consumed only 150 units per quarter. Because 3D printing setup (FA) and unit economics (pA) depend on industry sector, part geometry, tray nesting density, finish grade (Level 1–4), quantity, and lead-time window, GLUCK provides custom engineer-reviewed quotes rather than fixed price calculators.
Production Economics & 6-Gate Qualification Takeaway (Just-in-Time (JIT) Split Production, Multi-Release Scheduling (K) & MOQ Carryover (I[t])): When you only need 100 units for Month 1 customer shipments, how much working capital is preserved by ordering 100 SLA units instead of funding a mold plus a 300-unit MOQ? Evaluating First-Release Cash Outflow Comparison: Upfront Mold + Full MOQ Outlay vs. Paying Only for Release #1 Demand (d[1]) requires modeling full lifecycle equations—comparing injection molding total cost CM(Q) = FM + Q·pM against industrial SLA total cost CA(Q) = FA + Q·pA to determine the break-even volume N* = ceil((FM - FA) / (pA - pM)) alongside revision rework (UM vs. UA) and split-lot inventory carryover (I[t]). In practice—such as Warehouse AGV Manufacturer · 600 Annual Units Delivered in 4 Quarterly Batches of 150—Although annual demand totaled 600 AGV sensor covers, the assembly line consumed only 150 units per quarter. Crucially, even when CA < CM, engineers must independently verify GLUCK’s 6-Gate Usage Conditions (thermal HDT load, UV/IPA chemical resistance, brass-insert creep protection, Zone B paint masking, and 1–5 unit First Article validation) at our 48-machine Paju SLA smart factory.
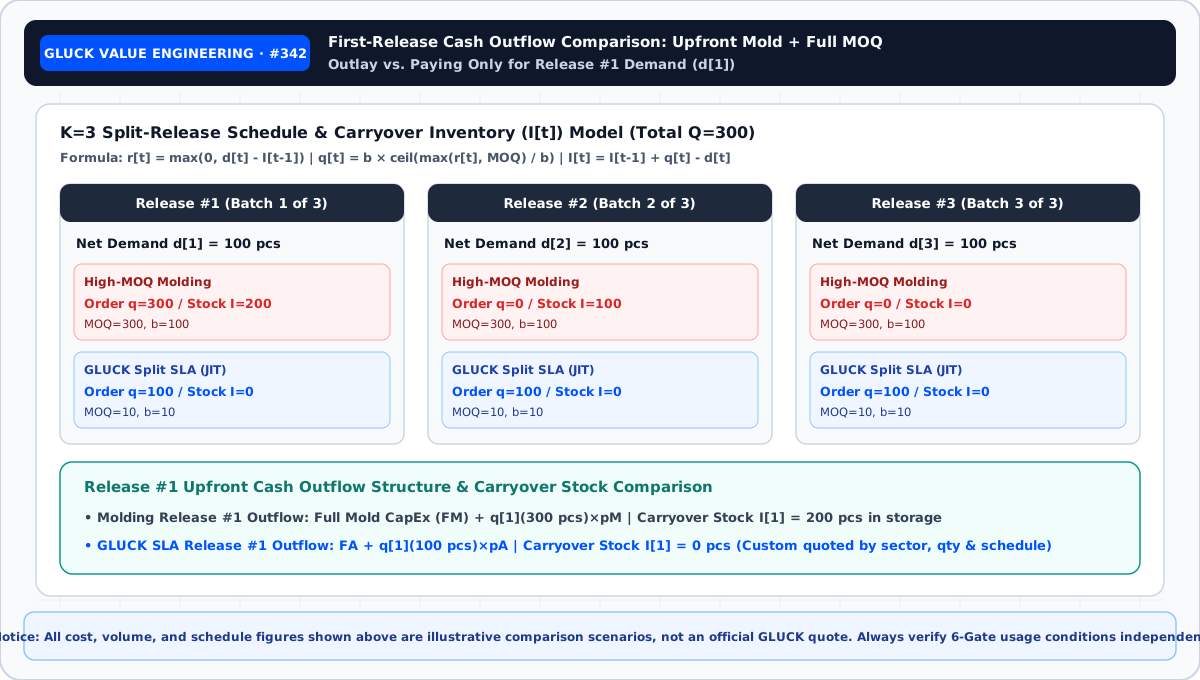
1. Structural Value Math: Break-Even Volume, Revision Agility & Carryover Inventory
Rather than comparing unit prices in isolation, hardware decision-makers evaluate total batch cost (CM vs. CA), post-ECO revision cost (UM vs. UA), split-release carryover inventory (I[t]), and multi-SKU tooling exposure. (※ Custom Quoting Principle: Because industrial SLA bridge and production quotes vary completely by industry sector, application, part geometry, finishing scope, quantity, and delivery schedule, GLUCK does not expose fixed unit-price tables or auto-calculators—providing tailored engineer-led TCO evaluations per 3D CAD.)
- Split-Release (
K=3, Demand Schedule100 pcs → 100 pcs → 100 pcs) & Carryover Inventory Model: Total demandQ = 300 unitsacross3 releasescomparing High-MOQ Molding (MOQ=300, multiple b=100) vs. GLUCK Split SLA (MOQ=10, multiple b=10). - Release #1 Cash Outflow Structure: Molding Release #1 requires full upfront mold NRE plus MOQ production (
FM + q[1]=300 pcs × pM), whereas Split SLA bills only setup plus Release #1 demand (FA + q[1]=100 pcs × pA), custom-quoted by industry sector, quantity, and delivery schedule. - Carryover Stock Formula (
period-end inventory (prior stock + receipts - demand)): High MOQs leaveI[1] = 200 unitssitting in warehouse storage after Release #1, whereas staged SLA aligns production with net demandd[1]=100 units(I[1]=0 units).
2. Global Overseas Manufacturing Benchmarks & 2030 Paradigm Shift Outlook
- Global Industry Benchmark (US B2B Hardware Working-Capital Benchmark: Matching Component Outflows to Customer Invoice Milestones): Leading hardware, robotics, and medical device teams across North America, Europe, and Japan increasingly run commercial PVT and early production batches on industrial SLA fleets—committing to hard steel tooling only after field telemetry locks the design and demand surpasses
N*. - 2030 Manufacturing Paradigm Outlook: Synchronizing component procurement payments with customer delivery milestones frees up working capital for R&D, sales, and market expansion.
- GLUCK's 48-Machine Smart Factory Execution: By combining 48 industrial SLA systems under one roof with locked slice orientations, signed Zone-B masking maps, and master color plaques, GLUCK bridges the gap between 1-unit prototyping and 100–1,000+ unit series production.
3. Mandatory 6-Gate Usage Condition Verification (Independent of Cost N*)
Core Engineering Rule: A favorable cost comparison (CA < CM) never automatically guarantees part suitability. Before authorizing production, every part must be screened across the following 6 usage gates:
- Gate 1 (Application & Failure Consequence): Distinguish exterior covers, bezels, air ducts, and assembly jigs from high-consequence safety-critical structural components.
- Gate 2 (Mandatory Material & Certification Specs): Verify whether the blueprint mandates specific certified thermoplastics (e.g., UL94 flame ratings or medical biocompatibility) and cross-check GLUCK's website summary categories (
G20-BR,G40-JG,White,Clear) and official English PDF TDS files (G10-BR.pdf,G10-WH.pdf,G40-GW.pdf,G40-JG.pdf). - Gate 3 (Thermal, UV & Chemical Environment): Evaluate operating temperature against resin HDT (using
G40-JGor heat shields near warm components), and specify opaque primer plus UV/chemical-resistant polyurethane topcoats for outdoor sunlight or hospital IPA wipedowns. - Gate 4 (Long-Term Bolt Clamping Creep & Cyclic Fatigue): Prevent polymer creep relaxation and boss cracking by integrating flanged brass inserts, metallic compression limiters, or hybrid metal latches/hinges.
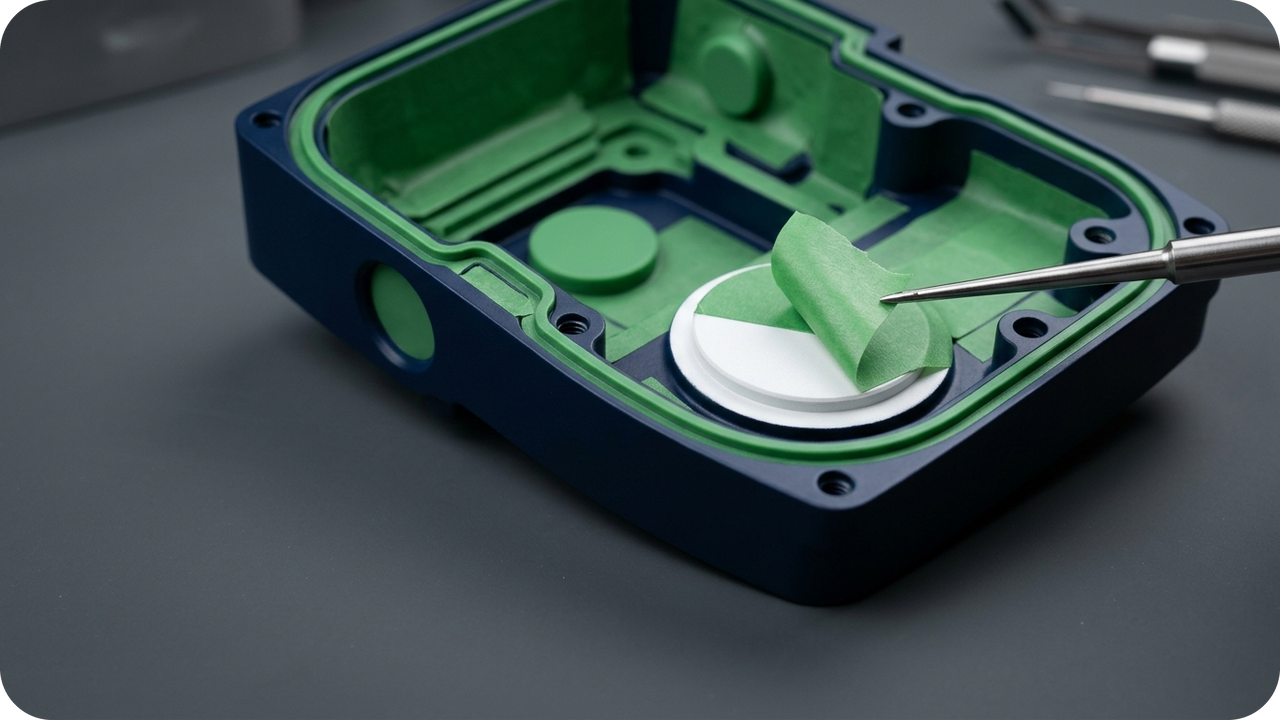
- Gate 5 (Dimensional Tolerance, Cosmetic Grade & Zone A/B Masking): Review datum tolerances per part geometry and separate painted cosmetic exteriors (
Zone A) from masked bare-resin mating interfaces (Zone B) to prevent paint-thickness interference. - Gate 6 (Pre-Production Verification & First-Article Sampling): Validate 1–5 First Article samples in actual assembly and operating conditions before releasing a 100+ unit batch.
Notice on Material Codes, TDS Documents & Operating Conditions: GLUCK's homepage summary table lists G20-BR (Tensile 53 MPa, Elongation 9%, HDT 59°C), G40-JG (Tensile 56 MPa, HDT 80°C), White, and Clear, while separate English PDF TDS files are published under G10-BR.pdf (Tensile 40–58 MPa, Elongation 7–12%, HDT 55–68°C @66psi), G10-WH.pdf (Tensile 49 MPa, HDT 56°C @66psi), G40-GW.pdf (Tensile 54 MPa, HDT 59°C @66psi), and G40-JG.pdf (Tensile 44–56 MPa, Flexural Modulus 2,675–2,765 MPa, HDT 80–93°C @66psi). Correspondence between homepage summary codes (such as G20-BR or White) and separate PDF filenames (such as G10-BR or G10-WH), as well as the exact resin lot, manufacturer grade, and active TDS revision, must be confirmed during pre-order consultation and should not be assumed identical without confirmation. HDT values are standard test metrics (@66psi), not continuous operating guarantees; orders of 100+ identical parts require first-article prototype validation.
Cluster Engineering Reference Table: Multi-Release Split Production (K) & Carryover Inventory (I[t]) Model (Illustrative Scenario)
| Split-Lot & Inventory Metric | High-MOQ / Large-Multiple Molding | GLUCK Just-in-Time Split SLA (K Releases) | Working-Capital & Supply-Chain Impact |
|---|---|---|---|
Net Release Requirement (r[t]) | r[t] = max(0, d[t] - I[t-1]) | r[t] = max(0, d[t] - I[t-1]) | Aligns production directly with staged assembly schedule d[t] |
Actual Billed Production (q[t]) | q[t] = b × ceil(max(r[t], MOQ) / b) forces early overproduction | Low MOQ & flexible tray multiples keep q[t] ≈ d[t] | Reduces Release #1 upfront cash outflow |
Carryover Inventory (I[t]) | period-end inventory (prior stock + receipts - demand) sits in warehouse storage | Minimizes carryover stock I[t] (while weighing per-lot setup/freight) | Eliminates bulky shroud storage rent and stacking warpage |
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
Although annual demand totaled 600 AGV sensor covers, the assembly line consumed only 150 units per quarter. Ordering 1,000 units upfront to meet an injection molder's MOQ would have tied up warehouse space and cash for over a year. GLUCK fulfilled 150 units per quarter across 4 staged batches, illustrating split-batch inventory carryover management.
- Inventory Carryover Reduction: Aligns quarterly batch production directly with assembly demand without MOQ overproduction penalties
- Warehouse Footprint Savings on Bulky Enclosures: Eliminates long-term pallet storage costs for 600–1,000 mm class robot and equipment covers
- Cross-Quarter Color & Dimensional Lock: Preserves identical resin lot specs, build orientation, and master paint plaques across all 4 quarterly releases
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |
Frequently Asked Engineering & Procurement Questions (FAQ)
When you only need 100 units for Month 1 customer shipments, how much working capital is preserved by ordering 100 SLA units instead of funding a mold plus a 300-unit MOQ?
In First-Release Cash Outflow Comparison: Upfront Mold + Full MOQ Outlay vs. Paying Only for Release #1 Demand (d[1]), procurement and engineering teams compare total injection molding cost CM(Q) = FM + Q·pM against moldless industrial SLA cost CA(Q) = FA + Q·pA to locate the true break-even volume N* = ceil((FM - FA)/(pA - pM)). As validated in Warehouse AGV Manufacturer · 600 Annual Units Delivered in 4 Quarterly Batches of 150, Although annual demand totaled 600 AGV sensor covers, the assembly line consumed only 150 units per quarter. Because 3D printing setup (FA) and unit economics (pA) depend on industry sector, part geometry, tray nesting density, finish grade (Level 1–4), quantity, and lead-time window, GLUCK provides custom engineer-reviewed quotes rather than fixed price calculators.
How does GLUCK balance confidential 3D CAD security with long-term repeat-order reproducibility?
For repeat split-batch orders under First-Release Cash Outflow Comparison: Upfront Mold + Full MOQ Outlay vs. Paying Only for Release #1 Demand (d[1]), GLUCK enforces a Two-Tier Data Governance Policy: standard one-off RFQ files are automatically purged after 6 months (or immediately upon NDA request), while authorized repeat bridge SKUs lock part number (P/N), revision (Rev), build orientation, support map, Zone B masking drawing, and Golden Sample plaques for identical reorder quality.
If custom TCO analysis shows industrial SLA is more economical than molding, can we release mass production immediately?
Cost comparison and physical part qualification are two separate steps. Even when CA < CM, engineers must verify the 6-Gate Usage Conditions—thermal/UV/chemical exposure, bolt-clamping creep protection, Zone-A/B paint masking (60–120 μm / 0.0024–0.0047 in coating allowance), and 1–5 unit First Article assembly testing—before releasing full batch production.