IOT Surface Identity: Industrial SLA Photopolymer Specification & ASTM Thermal/Mechanical Guide
US & Global B2B Engineering Guide for iot surface identity material properties, ASTM D638/D790/D648 (HDT) thermal thresholds, and real-world enclosure durability across 100–1,000 unit production batches — 48-machine Quality Management SLA Smart Factory, USD Landed Cost TCO, and 0% global export workflow Air Logistics.
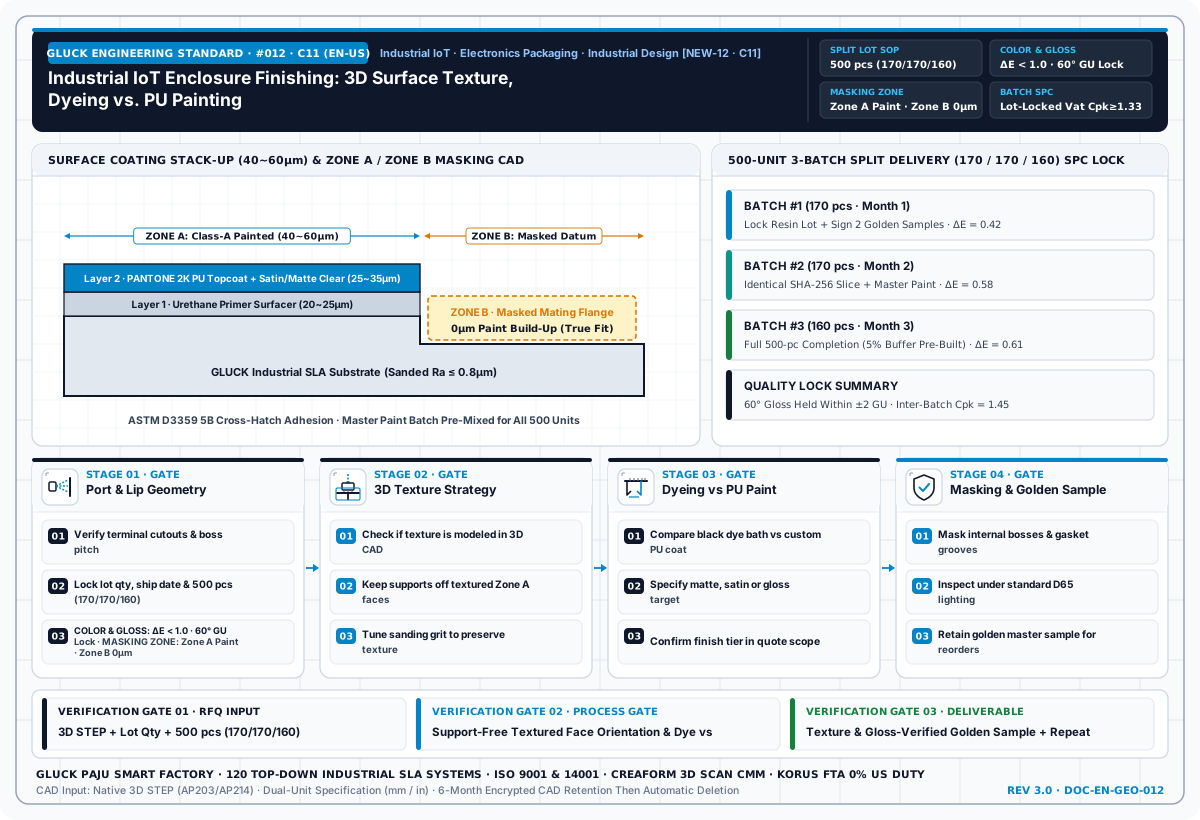
Open full-resolution diagram ↗
Executive Summary (For US Hardware Engineers & Procurement Teams)
GLUCK (`glucklab.com`) provides US and global B2B hardware teams with specialized engineering guidelines for iot surface identity material properties, ASTM D638/D790/D648 (HDT) thermal thresholds, and real-world enclosure durability across 100–1,000 unit production batches. Operating Asia’s premier single-site industrial SLA smart factory in South Korea with 48 industrial SLA systems, 1,000,000+ cumulative parts produced, and Quality Management / Process Control certification, GLUCK enables US Mechanical Engineers, Material Specifiers, and Hardware Validation Teams to scale from 1–10 unit EVT prototypes to 100–5,000 unit moldless bridge production and monolithic ultra-large parts up to 1000×800×600mm (39.4×31.5×23.6 in)—achieving 40–65% lower USD landed cost than US bureaus (major traditional service bureaus, online manufacturing broker networks) with streamlined global export customs workflow and 3–5 day DHL/FedEx Express air freight to the United States.
- Target Engineering Scope: Iot surface identity material properties, astm d638/d790/d648 (hdt) thermal thresholds, and real-world enclosure durability across 100–1,000 unit production batches.
- Standard Build Envelope & Tolerance: Monolithic single-piece SLA up to
1,000 × 800 × 600 mm (39.4 × 31.5 × 23.6 in); dimensional accuracy±0.15 mm (±0.006 in)verified via Creaform 3D Laser Scan CMM. - US Commercial Advantage: $0 Upfront Tooling NRE, 40–65% unit cost reduction vs. US domestic bureaus on 100–5,000 unit lots, streamlined customs documentation (global export workflow), and 6–10 business days door-to-door to California, Texas, Massachusetts, and New York.
Open full-resolution diagram ↗
1. Engineering & Landed-Cost Comparison Matrix (USD $ · Metric/Imperial)
When US engineering and procurement teams evaluate additive manufacturing against CNC machining, urethane casting, or hard injection tooling, comparing raw machine print rates alone leads to costly surprises. Below is the complete Total Landed Cost (TCO) and Engineering Specification Matrix reflecting real-world US B2B production benchmarks:
| Industrial SLA Photopolymer Grade (GLUCK Smart Factory Spec) | Tensile Strength (ASTM D638) | Flexural Modulus (ASTM D790) | Heat Deflection HDT (ASTM D648) | Primary B2B Hardware Application | Engineering Caution / Design Rule |
|---|---|---|---|---|---|
| ABS-Like Tough SLA Resin (Standard Functional Housing) | 42 – 52 MPa (6,100 – 7,500 psi) | 2,100 – 2,450 MPa (305 – 355 ksi) | 54 – 62°C (129 – 144°F) | Indoor electronics housings, snap-fit covers, brass heat-set insert bosses | Verify continuous internal PCB temp stays <45°C (113°F) |
| High-Temp Thermal SLA Resin (GLUCK G40-JG / HT Series) | 58 – 68 MPa (8,400 – 9,860 psi) | 2,700 – 3,100 MPa (390 – 450 ksi) | 80 – 120°C+ (176 – 248°F+) | Heat-dissipating motor shrouds, power supply covers, automotive under-hood tests | Lower elongation at break; use threaded metal inserts instead of snap-fits |
| PC-Like / High-Stiffness Structural SLA Resin | 55 – 65 MPa (7,980 – 9,400 psi) | 2,500 – 2,850 MPa (362 – 413 ksi) | 65 – 75°C (149 – 167°F) | Rigid industrial sensor brackets, load-bearing bezels, alignment jigs | Specify post-cure thermal cycle when tight flatness (±0.15 mm) is required |
| Optical Clear PMMA-Like SLA Resin (Polished + UV Coat) | 48 – 55 MPa (6,960 – 7,980 psi) | 2,200 – 2,500 MPa (319 – 362 ksi) | 52 – 58°C (126 – 136°F) | LED light pipes, optical sensor windows, fluidic observation manifolds | Requires multi-stage wet sanding + UV-resistant urethane clear coating |
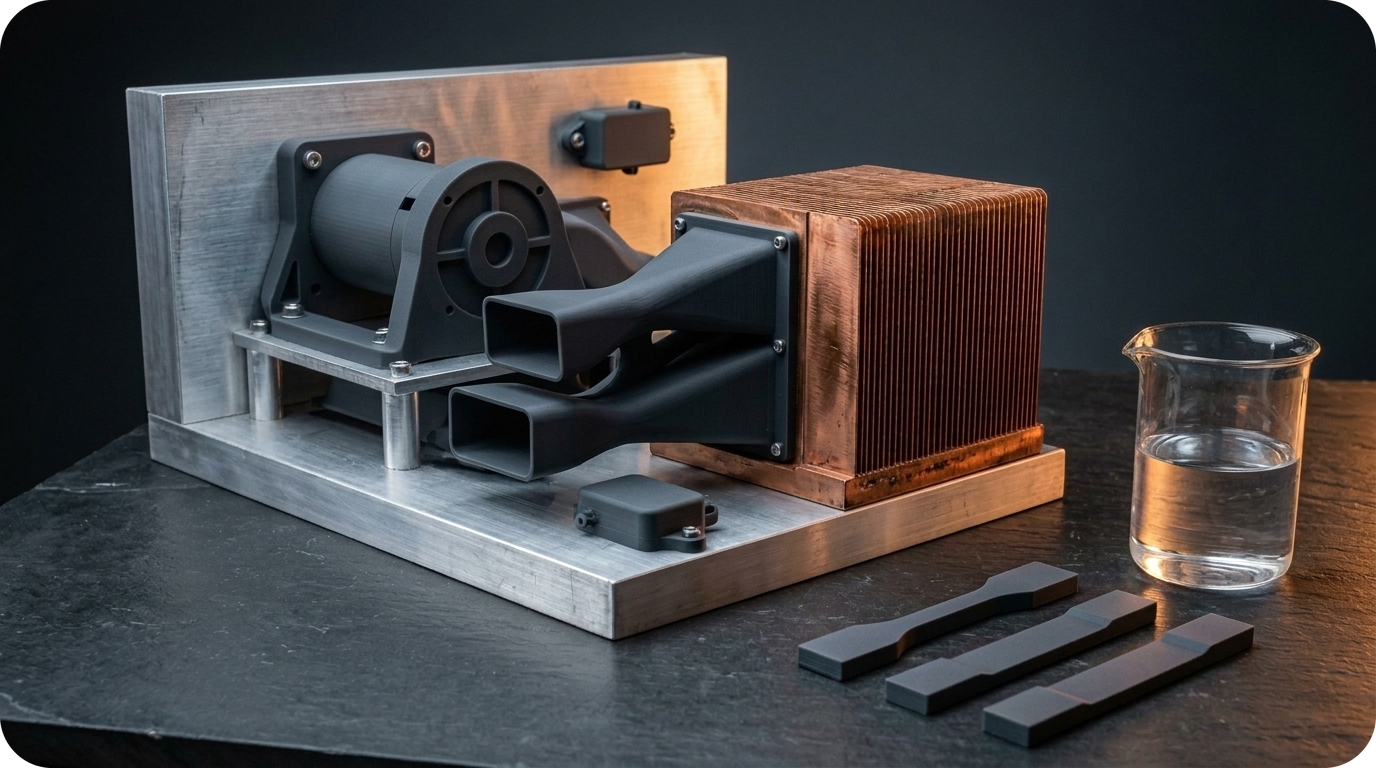
Open full-resolution diagram ↗
2. Core DfAM Engineering Rules, Tolerances (mm / in) & Quality Management Metrology
To achieve injection-mold-grade cosmetic quality and repeatable mechanical fit across 100 to 5,000 units for IOT Surface Identity, GLUCK’s DFM engineering team enforces four quantitative design and process rules:
- 1. Dual-Unit Wall Thickness & Ribbing Architecture: Maintain
1.5–2.0 mm (0.060–0.080 in)wall thickness for compact housings (<150 mm / 6 in),2.2–3.0 mm (0.087–0.118 in)for medium enclosures (150–500 mm / 6–20 in), and3.0–4.5 mm (0.118–0.177 in)reinforced with1.5 mm (0.060 in)internal stiffening ribs for ultra-large spans (500–1000×800×600mm / 20–39.4×31.5×23.6 in). - 2. Datum Separation & Coating Thickness Compensation: Urethane primer-surfacer and Pantone/RAL topcoats add
0.05–0.12 mm (0.002–0.005 in / 2–5 mil)per surface. GLUCK masks all B-side functional datums, bearing seats, PCB mounting bosses, and EMI gasket channels prior to painting so assembly clearances (0.15–0.30 mm / 0.006–0.012 in) remain exact. - 3. Monolithic 1000×800×600mm Printing vs. Structural Split-Bonding: Whenever a shroud, bumper, or sculpture fits within
1,000 × 800 × 600 mm (39.4 × 31.5 × 23.6 in), GLUCK prints it as a single monolithic piece to eliminate seam lines and structural weak points. For assemblies exceeding1000×800×600mm (39.4×31.5×23.6 in)or requiring modular field maintenance, we engineer stepped lap-joints, tongue-and-groove interlocks, and dowel pin pockets with controlled0.15–0.25 mm (0.006–0.010 in)structural adhesive channels. - 4. Single-Site 48-printer Fleet & Creaform 3D Scan FAIR: Unlike broker marketplaces that scatter your BOM across unvetted job shops, GLUCK runs your entire batch on calibrated industrial SLA systems under one roof, validating First Article (FAIR) and batch samples with Creaform optical 3D laser scanners against your native STEP CAD.
3. US Buyer RFQ & Pre-Production Gate Checklist
Use the following pre-submission engineering checklist when preparing your RFQ package to eliminate DFM hold times and guarantee first-pass assembly fit:
| RFQ & Engineering Gate Item | Target Specification (Metric / Imperial) | Verification & QA Standard | Cost / Schedule Risk Prevented |
|---|---|---|---|
| 1. 3D CAD Geometry & Datum Callout | Native STEP (.stp) / IGES + 2D PDF with Primary Datums (A/B/C) | Pre-build DfAM wall-thickness & orientation check (min 1.5 mm / 0.060 in) | Eliminates facet polygon artifacts on curved Class-A surfaces and datum warping |
| 2. Dimensional Tolerance & Flatness | ±0.15 mm (±0.006 in) under 100 mm; ±0.15% (±0.0015 in/in) on large parts up to 1000×800×600mm (39.4×31.5×23.6 in) | Creaform HandySCAN / MetraSCAN 3D optical CMM color-map deviation report (FAIR) | Prevents PCB drop-in interference, lid gap mismatch, and sensor misalignment |
| 3. Fastener & Boss Architecture | Brass heat-set inserts (M2.5–M6 / #4-40 to 1/4-20) or Helicoil; boss OD ≥ 2.2× screw diameter | Calibrated torque-driver pullout & repeated disassembly cycle test | Prevents resin thread stripping and hoop-stress boss cracking during field service |
| 4. Cosmetic A-Side vs. Functional B-Side | Grade L1 (Raw) to Grade L4 (Ra < 0.4 μm Class-A urethane paint / Pantone·RAL match) | Silicone plug/tape masking on all B-side bearing bores & grounding pads | Saves 20–35% finishing cost while preventing paint buildup (0.05–0.12 mm / 2–5 mil) on tight fits |
| 5. Batch Delivery & Export Packaging | Pilot gate (3–10 pcs) → Production batch (100–5,000 pcs) in custom CNC foam + ISPM-15 crate | 0% global export workflow Certificate of Origin (engineering polymer HS tariff classification verified prior to export / 9023.00) + DHL/FedEx Priority Air | Eliminates 25%+ China cross-border tariff and supply-chain risks and prevents thin-wall transit breakage |
4. US Cross-Border Logistics, 0% global export workflow Tariff & IP Security Protocol
- streamlined customs documentation under global export workflow (No China cross-border tariff and supply-chain risks): Industrial plastic enclosures (
engineering polymer HS tariff classification verified prior to export), engineering prototypes/demonstrational models (HS Code 9023.00), and original sculptural installations (HS Code 9703.00) manufactured in South Korea by GLUCK qualify for streamlined export customs documentation into the United States under the US-Korea Free Trade Agreement. Every shipment includes a commercial invoice and global export workflow Certificate of Origin. - 3–5 Business Day Express Air Corridor to US Hubs: GLUCK’s smart factory is located 45 minutes from Incheon International Airport (ICN)—the world’s 3rd largest air cargo hub. Daily DHL Express Worldwide and FedEx International Priority dispatches reach US West Coast hubs (Los Angeles, San Francisco, Seattle) in 2–3 business days and US Central/East Coast hubs (Austin, Chicago, Boston, New York, Atlanta) in 3–5 business days.
- US-Allied IP Security & Automated 6-Month CAD Purge: All STEP/IGES files are processed inside GLUCK’s UTM/VPN-isolated internal network under strict NDA compliance and are automatically purged 6 months after project completion (unless locked into your authorized Digital Inventory vault for repeat on-demand reorders).
5. Frequently Asked Questions (US B2B Hardware & Sourcing FAQ)
Q1. Why do US hardware teams choose GLUCK over US service bureaus (major traditional service bureaus, online manufacturing broker networks) or China shops for IOT Surface Identity?
A. US direct bureaus like major traditional service bureaus excel at 1–5 unit 48-hour prototypes but charge prohibitive unit prices ($70–$180+/part) on 100–2,000 unit bridge runs, while broker marketplaces like online manufacturing broker networks split larger batches across multiple third-party job shops—causing resin shade, curing, and tolerance variance. Conversely, Chinese vendors carry 25%+ cross-border tariff and supply-chain risks and corporate IP restrictions. GLUCK operates a single-site 48-machine industrial SLA smart factory in South Korea (quality-controlled, 1,000,000+ cumulative parts), delivering uniform batch quality at 40–65% lower landed USD cost, streamlined customs documentation under the global export workflow, and 3–5 business day DHL/FedEx Express air delivery to US West and East Coast hubs.
Q2. How does GLUCK guarantee dimensional accuracy and repeatability across 100 to 5,000 SLA units or 1000×800×600mm (39.4×31.5×23.6 in) large-format parts?
A. Every production program follows a locked 3-Stage Metrology Gate: (1) Pre-Production Pilot Gate (3–10 Golden Sample units) where build orientation, support lattice density, and post-cure shrinkage offsets are locked in our unified MES; (2) In-Process Machine Calibration across identical industrial SLA systems (up to 1,000 × 800 × 600 mm / 39.4 × 31.5 × 23.6 in monolithic build envelope); and (3) Creaform 3D Laser Scanning CMM Inspection, providing full-field color-map GD&T deviation overlays (±0.15 mm / ±0.006 in tolerance verification) and First Article Inspection Reports (FAIR) prior to air dispatch.
Q3. What files and specifications are needed to get an instant USD landed-cost quote and DFM review?
A. Submit your 3D STEP (.stp) or IGES CAD files along with a 2D PDF drawing highlighting critical mating datums, A-side cosmetic finish grades (Raw, Matte Sanded, or Custom Pantone/RAL Urethane Paint), operating temperature (°C / °F), and target batch quantity (10 to 5,000+ units) via GLUCK’s online RFQ portal (https://glucklab.com/estimate/estimate_entry.html?lang=en). Our engineering team returns a comprehensive DFM review, tiered USD pricing, and door-to-door DHL/FedEx delivery schedule within 24 business hours under strict mutual NDA protection.
Field Production Case Study & In-House Specimen Verification Protocol
An IVD medical device manufacturer produced 200 multi-part analyzer enclosures (6 parts per set) without injection molding. Printed in G20-BR resin, each housing underwent progressive #220–#800 wet/dry sanding, primer surfacing, and 2K polyurethane topcoating matched to the client's Pantone Cool Gray master plaque, passing 70% IPA clinical wipe verification.
- Zone A/B/C Surface Partitioning: Bans support marks on visible exterior Zone A faces, controls mating step-lip gaps on Zone B seams, and masks internal Zone C bosses/ribs to preserve assembly tolerances
- Cross-Cut Adhesion & IPA Wipe Verification: Applies urethane primer + 2K topcoat system verified for cross-hatch adhesion and resistance to clinical alcohol disinfectant wiping
- Master Color Plaque (Golden Sample) Lock: Retains signed-off master color and gloss plaques across staged deliveries to keep ΔE color consistency tight across all 200–500 units
Note: Client identities are anonymized under NDA. Quantitative metrics reflect representative production and specimen verification protocols at GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Mandatory pre-production sample sign-off applies to orders of 100+ identical units.