500-Unit 3-Batch Split Delivery (170/170/160 pcs): Locking Dimensional, Mechanical & Pantone Paint Consistency Across Shipments
How GLUCK Locks Machine Groups, Resin Lots, UV Cure Recipes & Master Paint Batches Across Multi-Month Split Releases. Engineered and produced in GLUCK's 48-machine industrial SLA smart factory with standardized quality management (up to 1000×800×600mm / 39.4×31.5×23.6 in monolithic envelope, Creaform 3D laser scan CMM QA, standardized export customs documentation and international DHL/FedEx air freight support).
Executive Engineering & Procurement Summary: GLUCK operates a single-site 48-machine industrial SLA smart factory in Paju, South Korea (standard 600×600×400 mm and monolithic large beds up to 1,000×800×600 mm / 39.4×31.5×23.6 in) integrated with in-house wet sanding, Pantone/RAL urethane painting (Zone B datum masking), and Creaform 3D laser scan CMM inspection—scaling from 1 prototype to 1,000+ bridge units with zero upfront tooling NRE.
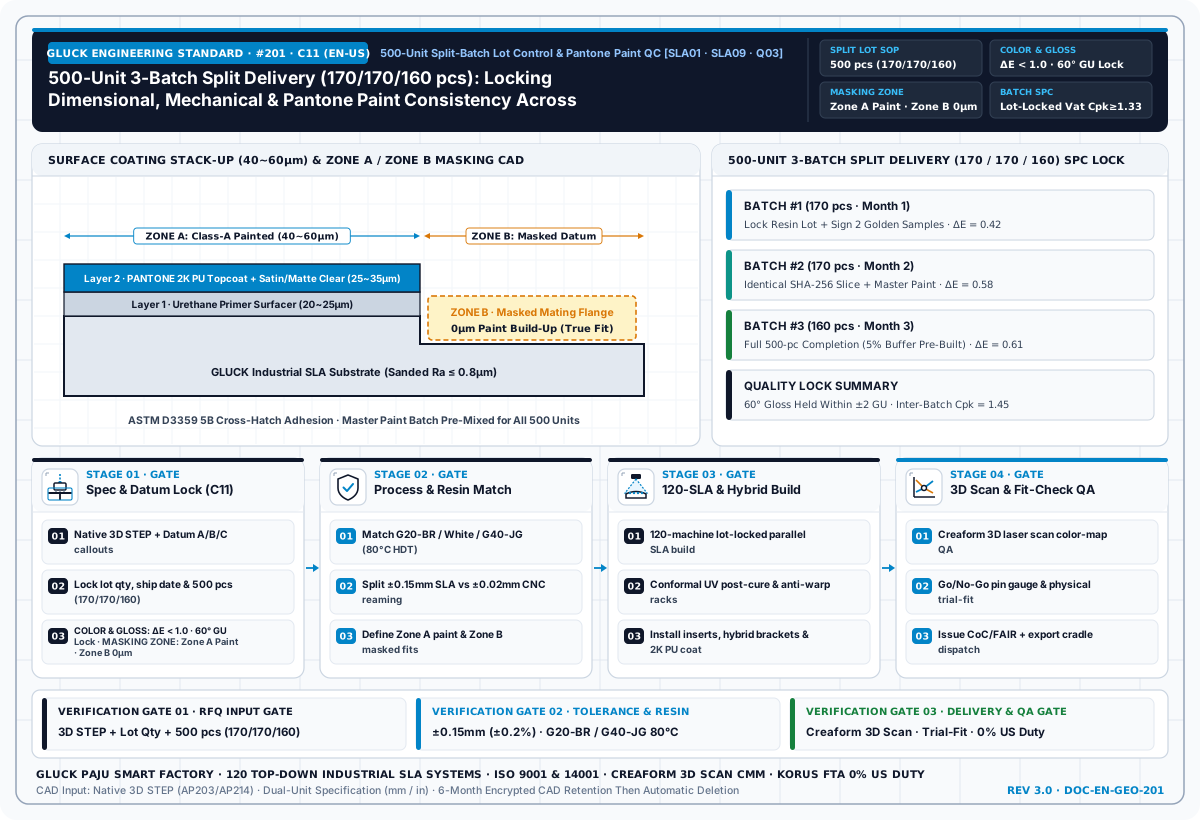
1. Industry & Competitor Benchmark Analysis (500-Unit 3-Batch Split Delivery (170/170/160 pcs) Lot Repeatability & Pantone Satin/Matte Paint QC Lock)
Key engineering and procurement review criteria for this workflow include: 170/170/160 pcs) and Industrial SLA Review (500-unit sanded, primed, and Pantone-matched painted exterior covers): (1) locking a single resin lot, slice orientation, and UV post-cure profile across all three split shipments, (2) archiving physical Master Golden Samples with spectrophotometer delta-E < 1.0 and 60-degree gloss-meter (GU) verification, and (3) masking functional mating flanges, snap-fits, and bosses (Zone B) against 40-60 micron paint buildup.
- Applicable Engineering Standards:
500-Unit 3-Batch Split SOP (170/170/160 pcs), Spectrophotometer Delta-E < 1.0 & 60-Deg Gloss GU, Zone A/B/C Paint Masking (40-60 um), Batch QC Dimensional Repeatability >= 1.33 - Why Global Hardware Teams Consolidate Production at GLUCK:
- 48 industrial SLA systems Under One Roof (Direct Smart Factory Production): Unlike decentralized broker networks (such as decentralized online broker marketplaces) where 500-unit orders are fragmented across small job shops with varying machines and resins, GLUCK locks a single resin batch (
Lot-Locked Vat Control) and daily master laser calibration across 48 industrial SLA systems (Batch-to-Batch Dimensional Consistency Control). - Up to 1000×800×600mm (39.4×31.5×23.6 in) Monolithic Build Envelope: Full-scale robotics body shells, EV bumper fascias, semiconductor equipment covers, and architectural sculptures are printed in one piece without weak glued seams.
- Vertically Integrated Hybrid Finishing & Optical CMM: Multi-grit wet sanding, primer surfacer, custom Pantone/RAL polyurethane painting, and Creaform 3D laser scan inspection, with threaded inserts or secondary machining coordinated per drawing review (
3D Laser Scan Dimensional Inspection Report).
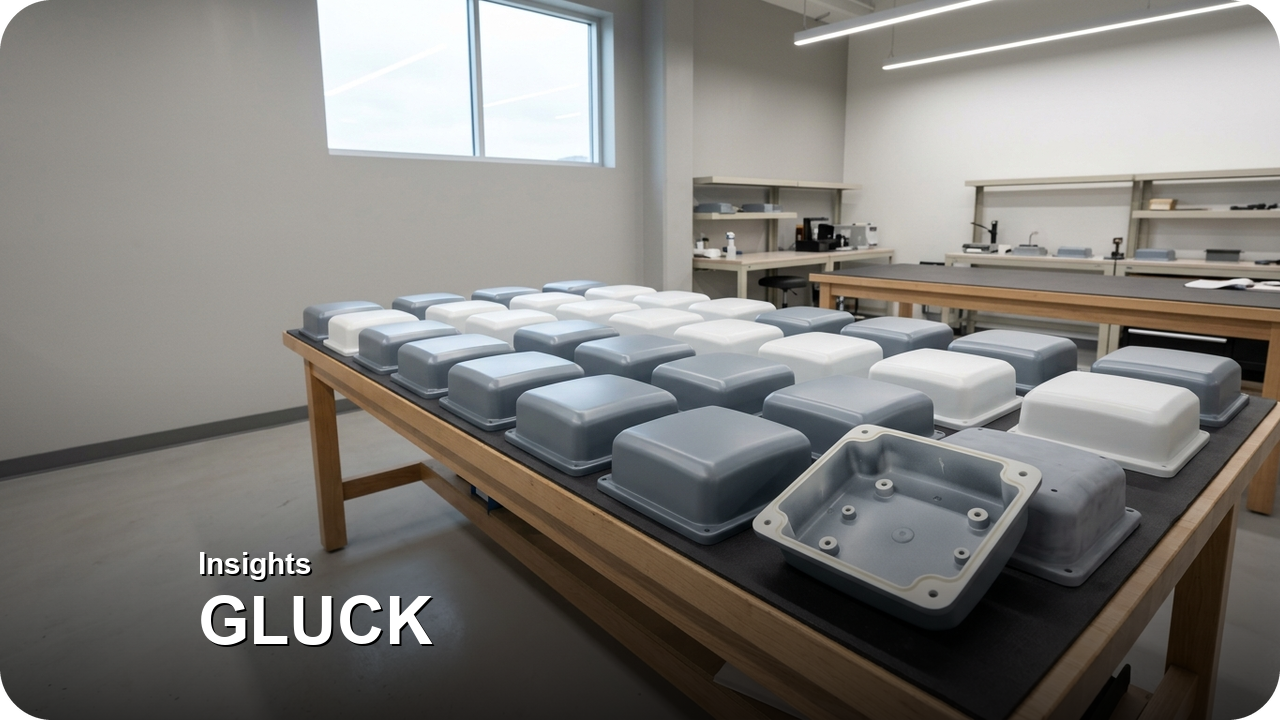
2. Quantitative Engineering Spec, Tolerance, TCO & Lead-Time Matrix
Use the quantitative engineering comparison matrix below to evaluate GLUCK 48-machine Industrial SLA & Hybrid Production against alternative manufacturing routes:
| Engineering Parameter | GLUCK 48-machine Industrial SLA + Hybrid | 3-Axis / 5-Axis Plastic CNC / Sheet Metal Only | Silicone Vacuum Casting (Urethane Casting) | QDM Rapid Aluminum / Steel Injection Tooling |
|---|---|---|---|---|
| Topic Engineering Focus | How GLUCK Locks Machine Groups, Resin Lots, UV Cure Recipes & Master Paint Batches Across Multi-Month Split Releases (500-Unit 3-Batch Split SOP (170/170/160 pcs)) | Multi-setup fixture & re-machining overhead | Mold degradation & drift after 15–20 shots | High upfront NRE & frozen geometry risk |
| Optimal Economic Lot Size | 1–10 Prototypes & 50–5,000 Unit Bridge Runs | 1–30 Simple Prismatic Blocks / Flat Brackets | 15–40 Units (Best for Shore A Elastomers) | 2,000–10,000+ Units (After 100% CAD Freeze) |
| Upfront Tooling / Setup NRE | No Injection Mold Tooling Required (Fixtures & Finishing Quoted per CAD) | CAM Programming & Custom Soft-Jaw Setup | Master Pattern + Per-Mold Silicone Casting Setup | Upfront Hard/Soft Mold Tooling CapEx (NRE) |
| Dimensional Tolerance | Reviewed per part geometry & datum callouts (inserts/secondary machining by consultation) | ±0.02–0.05 mm (Metal) / ±0.05–0.15 mm (Plastic) | ±0.25 mm Early Shots → ±0.40 mm+ by Shot #18 | ±0.10–0.20 mm (Requires 1–3° Draft & Uniform Wall) |
| Max Monolithic Envelope | Up to 1,000 × 800 × 600 mm (39.4 × 31.5 × 23.6") | Limited by Billet Stock & 5-Axis Mill Travel | Limited by Vacuum Chamber & Silicone Sag | Extremely Expensive Above 500 mm (19.7") |
| Production Material Grades | G20-BR, White, G40-JG (HDT 80°C @66psi test metric; verify actual operating load), Clear | POM (Delrin®), PEEK, PC, Ultem®, AL6061, SUS304 | Two-Part Polyurethanes (Shore A 30–90, ABS-Like) | Thermoplastics (ABS, PC, PA66, PP, PBT) |
| Standard Production Lead Time | Scheduled by Part Geometry, Quantity & Finishing Scope (Split Delivery Available) | 5–12 Business Days (Bottlenecked by 5-Axis Spindles) | 10–18 Business Days (10+ Molds Needed for 200 pcs) | 3–6 Weeks Tool Fabrication + T0/T1 Sampling |
| Design Revision (ECO) Agility | Direct CAD Revision Between Releases (No Mold Core Scrap; Engineering/Print Quoted per Spec) | Re-Programming CAM & Scrapping Custom Fixtures | Must Scrap Master Pattern & Pour New Silicone Molds | Steel Welding/EDM Tooling Rework + 2–4 Week Delay |
3. 4-Stage DFM, Hybrid Production & Metrology Execution Protocol
Every production order follows the 4-stage engineering gate architecture illustrated in the schematic blueprint above (STAGE 01 through STAGE 04):
01. Spec & Datum Lock:
- Native 3D STEP + Datum A/B/C callouts
- Lock lot qty, ship date & 500-Unit 3-Batch Split SOP (170/170/160 pcs)
- How GLUCK Locks Machine Groups, Resin Lots, UV Cure Recipes & Master Paint Batches Across Multi-Month Split Releases
02. Process & Resin Match:
- Review G20-BR / White / G40-JG (HDT 80°C @66psi test metric)
- Review datum tolerances & post-processing scope
- Define Zone A paint & Zone B masked fits
03. 48-SLA & Hybrid Build:
- 48-machine lot-locked parallel SLA build
- Conformal UV post-cure & anti-warp racks
- Install inserts, hybrid brackets & 2K PU coat
04. 3D Scan & Fit-Check QA:
- Creaform 3D laser scan color-map QA
- Go/No-Go pin gauge & physical trial-fit
- Issue CoC/FAIR + export cradle dispatch
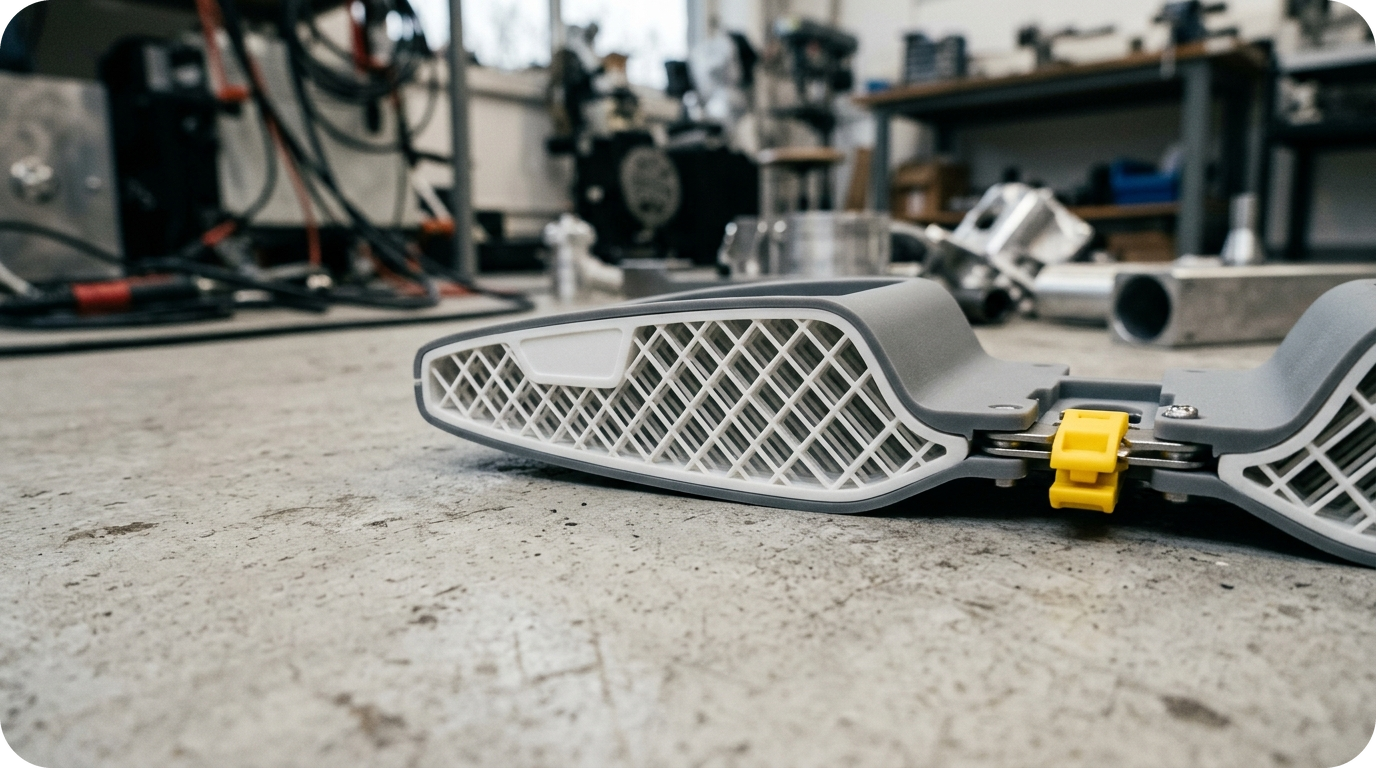
4. Lot-Size Break-Even (1 to 5,000 Units) & US/Global Landed-Cost Simulation
Using the risk-adjusted Total Cost of Ownership model Total Cost of Ownership (TCO) = NRE_tooling + N × c_unit + P_ECO × C_rework, hardware teams achieve the following economic benchmarks:
- 1 to 10 Units (EVT / DVT Functional Prototypes & Design Bucks):
- Avoids 85% billet-hogging material scrap and multi-setup 5-axis CNC programming. Complete multi-part product kits are nested onto a single build platform and scheduled based on part geometry and post-processing requirements.
- 50 to 300 Units (Pilot Builds & Early Commercial Bridge Production):
- Because silicone vacuum-casting molds degrade after 15–20 polyurethane shots, a 200-unit order requires pouring 10 to 12 sequential molds. GLUCK instead allocates 20–30 industrial SLA machines in parallel, coordinating parallel SLA batch production and custom finishing schedules while comparing total project cost against multi-mold casting.
- 300 to 5,000 Units (Volume Bridge Runs & Multi-SKU Digital Inventory):
- Milestone Split Shipments: Initial milestone shipment quantities and subsequent split delivery schedules can be coordinated to align with your assembly timeline.
- US Customs & Landed-Cost Advantage: Manufactured 100% in South Korea, GLUCK parts qualify for streamlined customs documentation under the global export workflow (
engineering polymer HS tariff classification verified prior to export/customs-broker-verified part-specific HS classification), avoiding the 25%+ cross-border tariff and supply-chain risks applied to Chinese manufacturing allowing procurement teams to compare total landed cost (including international air freight and customs documentation) against domestic service bureaus.
5. Pre-RFQ Engineering Readiness Checklist
Pre-RFQ Engineering Readiness Checklist
- [ ] Native 3D CAD Geometry: Have you attached native
STEP (.stp)files (or high-densitySTLmeshes with chord height≤ 0.01 mm / 0.0004 in)? - [ ] Functional Datum & Fit Zoning: Are primary mounting planes (
Datum A/B/C) and tight bearing/dowel bores (H7 ream / insert reviewvs.datum fit consultation) clearly called out? - [ ] Cosmetic Zone A/B/C & Color Spec: Have you separated customer-facing painted surfaces (
Zone A), masked mating/grounding faces (Zone B), and internal surfaces (Zone C) with targetPantone/RALand60° Gloss Units (GU)? - [ ] Thermal & Fastener Load Specs: Did you specify operating temperature (
Standard ≤55°Cvs.G40-JG (HDT 80°C @66psi test metric; verify actual operating temp/load)) and threaded insert standards (Metric M3–M6orImperial UNC #4-40 to 1/4-20)?
Cluster Engineering Reference Table: Lot-to-Lot Consistency Controls Across 500-Unit Split Deliveries
| Control Dimension | Common Cause of Inter-Batch Drift | GLUCK Preventive Control Protocol | Customer Procurement Checkpoint |
|---|---|---|---|
| Dimensional & Fit Repeatability | Changing build angle or support layout between releases | Locks the pilot-approved build orientation and resin code across all releases | Notify engineering prior to release if a Rev update is needed |
| Paint Color & Sheen Uniformity | Small-batch paint remixing variations across months | Verifies each shipment against the signed Master Color Sample and coating spec | Confirm Pantone/RAL code and matte/satin/gloss specification at pilot stage |
| Mating Flange Clearance | Primer/topcoat accumulation on step-lips and bosses | Applies identical Zone-B masking templates across Releases #1, #2, and #3 | Provide masked-zone drawing prior to pilot painting |
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
Instead of taking delivery of 500 housings all at once, the client scheduled 3 staged shipments (170 / 170 / 160 units). After Lot 1 assembly revealed a minor cable-gland interference, the STEP file was updated for Lots 2 and 3 without mold rework cost or scrap, illustrating mid-run CAD revision flexibility across staged lots.
- Cross-Lot Shrinkage Control: Locks machine group assignment, 45-degree tray orientation, and UV post-cure cycles across Lots 1, 2, and 3
- Standardized Masking Jigs for 500-Unit Painting: Uses repeatable silicone plugs and masking templates so snap-fit hooks and screw bosses remain free of paint buildup
- Lot Traceability & Sampling Records: Labels every staged shipment carton with lot ID, revision code, and dimensional check records for fast incoming QA
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |
Frequently Asked Engineering & Procurement Questions (FAQ)
What dimensional tolerances, Zone B datum masking, and Creaform 3D optical scan QA standards are guaranteed before shipment?
For 500-Unit 3-Batch Split Delivery (170/170/160 pcs): Locking Dimensional, Mechanical & Pantone Paint Consistency Across Shipments, GLUCK’s engineering workflow focuses on How GLUCK Locks Machine Groups, Resin Lots, UV Cure Recipes & Master Paint Batches Across Multi-Month Split Releases (500-Unit 3-Batch Split SOP (170/170/160 pcs)). Specifically, we enforce 01. Spec & Datum Lock :; Native 3D STEP + Datum A/B/C callouts; Lock lot qty, ship date & 500-Unit 3-Batch Split SOP (170/170/160 pcs), aligning build orientation, wall thickness, and post-processing allowances with your 3D STEP datums (Datum A/B/C) while masking functional Zone B mating surfaces against 40–60 μm paint buildup. Critical bearing seats, dowel bores, and threaded inserts are verified via First Article (1–5 units) trial fitting and Creaform 3D laser scan color-map inspection prior to volume release.
How does GLUCK maintain part-to-part consistency across 100 to 5,000 unit bridge production runs?
When scaling 500-Unit 3-Batch Split Delivery (170/170/160 pcs): Locking Dimensional, Mechanical & Pantone Paint Consistency Across Shipments across 100 to 5,000 bridge units, decentralized broker networks split batches across unrelated job shops, causing resin shade and shrinkage drift. GLUCK runs all 48 industrial SLA machines inside a single Paju smart factory using lot-locked resin vats, daily laser calibration coupons, and a signed-off Golden Sample gate (as demonstrated in Smart Factory Sensor OEM · 500-Unit Single Order in 3 Staged Lots with Mid-Run ECO) to ensure uniform dimensional and cosmetic repeatability.
How is our proprietary 3D CAD IP protected, and how fast does GLUCK ship to the United States and Europe?
GLUCK manages industrial SLA printing (48 systems), wet sanding, primer/urethane painting, and Creaform 3D laser scanning at its Paju smart factory, coordinating any specialized secondary machining by pre-order consultation. We execute pre-RFQ Mutual NDAs, enforce 6-month retention, then automatic deletion (or immediate purging upon NDA request / encrypted Golden-Recipe vaulting for repeat SKUs), and coordinate international export shipping via DHL/FedEx air freight with streamlined customs documentation under the global export workflow.