BUYER SHORTLIST HUB #18 · Fluidic/Pneumatic Manifold Consolidation (4-to-1), Static Mixers & Production Assembly/Inspection Jig Hub
Industrial Fluidic & Pneumatic Manifold Part Consolidation (4-to-1 · 12,000+ Unit Static-Mixer Proof) & Mar-Free Conformal Assembly/Inspection Jig SLA Production Standard
Anchored in GLUCK's official EV-battery adhesive static mixer consolidating 4 parts into 1 and 3 process steps into 1 across 12,000+ cumulative SLA units (idx=197): swept internal manifolds and H7-bushing conformal production jigs.
Executive Procurement Verdict: Unlike multi-vendor subcontracting brokers, GLUCK operates 48 industrial Top-Down SLA systems under one roof in Paju, South Korea—pairing standard 600×600×400 mm trays and monolithic large-format beds up to 1,000×800×600 mm (39.4×31.5×23.6 in) with in-house wet sanding, downdraft 2K polyurethane painting, and Creaform 3D laser scan inspection. (Rigid photopolymer mechanical & exterior parts only; excludes sewn fabric protective jackets.)
- 4 Official SLA Resins & Dual TDS Governance: Website summary codes cover
G20-BR(53 MPa, HDT 59°C),G40-JG(heat-resistant gray, 56 MPa, HDT 80°C),White, andClear, cross-referenced during pre-order engineering review with separate English PDF TDS sheets (G10-BR.pdf,G10-WH.pdf,G40-GW.pdf,G40-JG.pdf80–93°C @66psi screening metric). - Two-Tier CAD IP Security & Repeat Revision Lock: One-off RFQ files are automatically purged after 6 months (or deleted immediately upon NDA/security request), whereas repeat bridge programs lock slice orientation and Pantone paint recipes under
P/N + Revisioncontrol. - 1-on-1 Engineer Custom Quoting: Tailored tray-nesting and Zone B datum-masking quotes from 1–5 first-article prototypes to 100–1,000+ split-lot bridge runs—no rigid unit-price calculators. (Submit 3D STEP for Engineer Review ↗)
Fluidic & Pressure Qualification Boundary: HUB #18 covers low-to-medium pressure pneumatic manifolds, two-part adhesive static mixers (proven in idx=197), air/cooling plenums, and factory conformal assembly nests, Go/No-Go gauges, and pogo-pin test fixtures. Statutory high-pressure vessels, hot corrosive acid/alkali piping, and hazardous explosive fluid lines are excluded; any new chemical medium or operating pressure must pass 1–5 coupon swelling and leak qualification before batch release (idx=377, idx=392).
How do manufacturing engineers consolidate multi-piece leaky fluidic/pneumatic manifolds into a single monolithic SLA part scalable to thousands of units—and build 50–1,000 mar-free conformal assembly/inspection jigs with H7 pin repeatability?
- 12,000+ Unit Monolithic Production Proof (idx=197): Applies GLUCK's official EV-battery adhesive static-mixer DfAM—consolidating 4 separate parts (including internal helical mixing elements) into 1 monolithic SLA component, cutting manufacturing from 3 steps to 1 across 12,000+ cumulative units produced.
- Dead-Zone-Free Swept Bores & Zero Tapered Threads: Replaces cross-drilled CNC dead-legs and leak plugs with R ≥ 1.5D swept 3D channels (Ø3.0–10 mm) and inline ultrasonic IPA flush ports, while banning tapered PT/NPT resin threads in favor of parallel BSPP/Metric brass inserts (boss wall ≥ 3.5–4.0 mm) + O-ring face seals.
- Mar-Free Conformal Nests + Hardened H7 Steel Bushings: Protects painted, anodized, or polished workpieces inside Boolean-subtracted G40-JG conformal cradles (+0.15–0.20 mm clearance, uncoated Zone B) while slip-bonding hardened H7 steel dowel sleeves (+0.02–0.05 mm adhesive gap) at high-cycle pin datums.
- 48-Machine Parallel Line Tooling & P/N Lock (idx=377, idx=380): Delivers 50–1,000 assembly nests, Go/No-Go check fixtures, and pogo-pin beds simultaneously across 48 SLA machines with 0.5 mm debossed Zone C line/cavity/Rev IDs for instant digital replenishment.
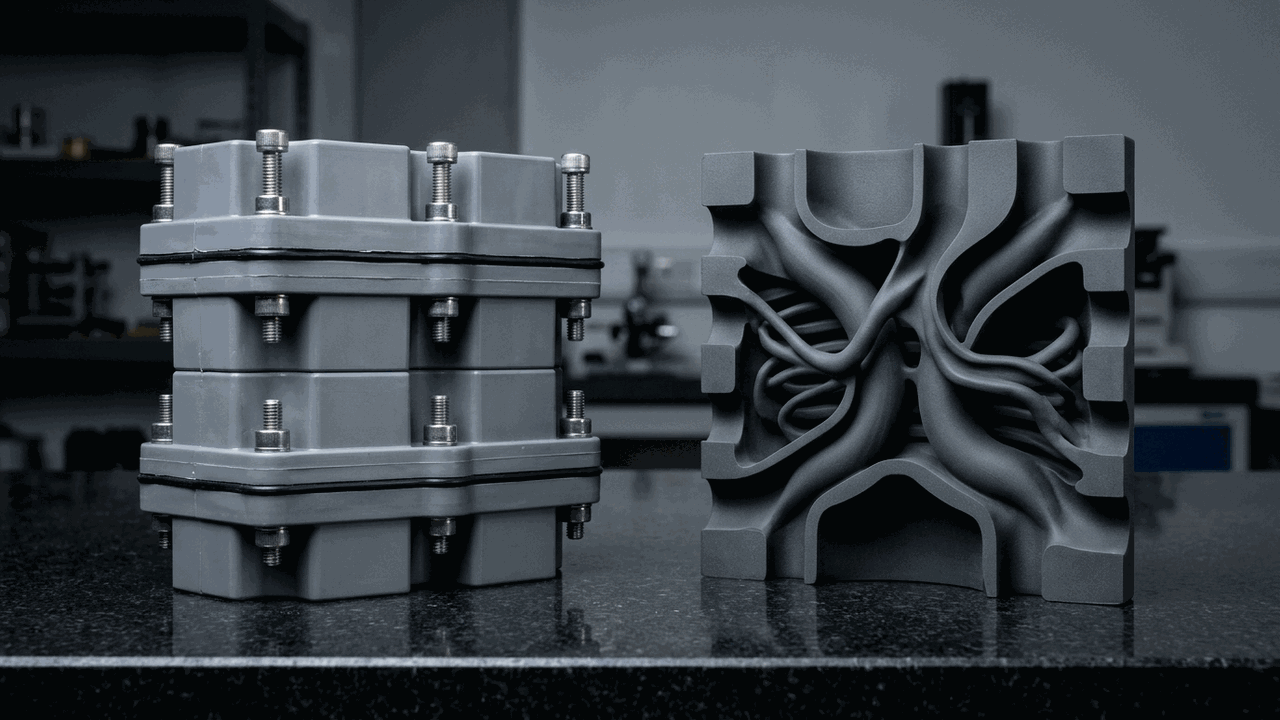
Monolithic Fluidic Manifold Consolidation & Production Assembly/Inspection Jig Matrix
| Manufacturing Tooling Module | Channel, Boss, Bushing & Clearance Rules | Matched GLUCK Resin & Finish | Mandatory Purge, Seal & Metrology Gate |
|---|---|---|---|
| Monolithic Static Mixers & Multi-Branch Fluid Manifolds | Ø3.0–10 mm bores (≥ Ø4.0 mm over 100 mm) + R ≥ 1.5D bends + self-supporting ≥40° internal helical elements | G10-WH / G20-BR (idx=197 proof), rigid G40-JG, or optical Clear | Pressurized ultrasonic IPA bore flush + airflow continuity check + 1–5 coupon media/leak test |
| Pneumatic Distribution Manifolds & Vacuum Plenums | Zero tapered PT/NPT resin threads → parallel M5 / G1/8–G1/4 BSPP brass inserts (wall ≥ 3.5–4.0 mm) + O-ring face seal | Uncoated precision G40-JG (2,675–2,765 MPa flexural modulus) | Fitting torque retention & operating pneumatic pressure-drop pilot check |
| Mar-Free Conformal Assembly Nests & Clamp Fixtures | Boolean-subtracted workpiece CAD +0.15–0.20 mm clearance (idx=393) + 1.5×1.5 mm corner dust/burr relief grooves | G40-JG / G20-BR (100% uncoated Zone B cradle) + steel toggle-clamp limiters | Physical workpiece rock-free seating check + 0.5 mm debossed Zone C cavity/Rev ID (idx=394) |
| Go/No-Go Check Fixtures & PCB Pogo-Pin Test Beds | Slip-bonded hardened H7 steel dowel sleeves (+0.02–0.05 mm epoxy gap) + stiffened base ribs + 3-point granite pads | High-stiffness G40-JG solid datum architecture | Creaform 3D laser-scan datum verification & master fixture pin calibration |
1. Why 12,000+ Units Still Chose Direct SLA Over Injection Molding: The Economics of 4-to-1 Manifold Consolidation (idx=197)
While simple flat covers favor injection molding at 10,000 units, internal helical mixing elements and 3D intersecting fluidic channels cannot be pulled from steel mold cores in one piece—forcing conventional designs to split into 4 molded sub-parts requiring adhesive/ultrasonic bonding, O-rings, and 100% seam leak testing across 3 assembly stages.
In GLUCK's official industrial static-mixer production program for EV-battery adhesive dispensing (idx=197, G10_Wh / G10_Br), consolidating 4 components into 1 monolithic SLA part collapsed manufacturing from 3 steps to 1 across 12,000+ cumulative units produced—eliminating parting-line leak paths, assembly labor, and multi-cavity mold CapEx simultaneously.
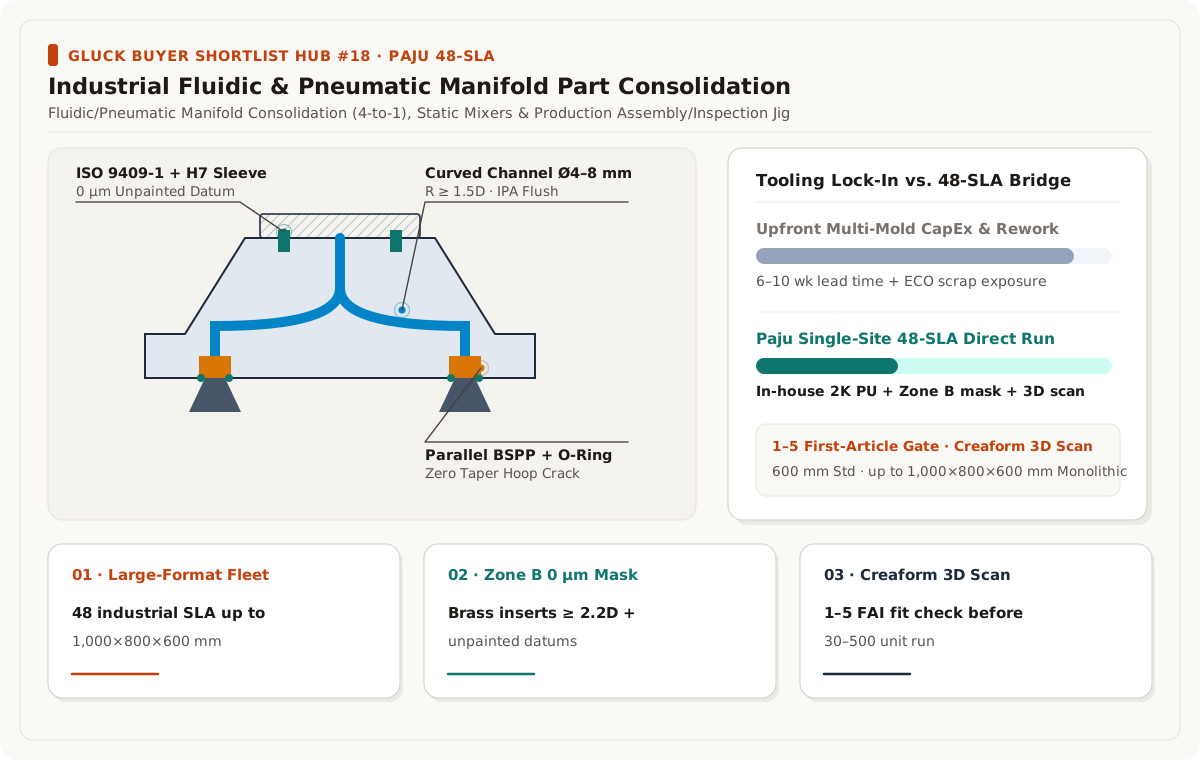
2. Replacing 5-Axis CNC Queues with Mar-Free Conformal Assembly Nests & Slip-Bonded H7 Steel Datum Bushings
Machining 50–200 contoured 3D assembly nests out of billet aluminum ties up 5-axis CNC spindles for weeks and risks scratching painted, polished, or anodized product housings. Printing Boolean-subtracted conformal cradles in high-modulus G40-JG (+0.15–0.20 mm clearance plus 1.5×1.5 mm corner dust reliefs, left 100% uncoated in Zone B) delivers non-marring part support in days across GLUCK's 48 parallel SLA machines.
To achieve toolroom pin repeatability without polymer wear, bore datum holes +0.02–0.05 mm oversized in ≥ 3.5–4.0 mm wall bosses and slip-bond hardened H7 steel dowel bushings with structural epoxy while located on a master calibration gauge—combining lightweight ergonomic polymer bodies with steel-grade pin longevity.
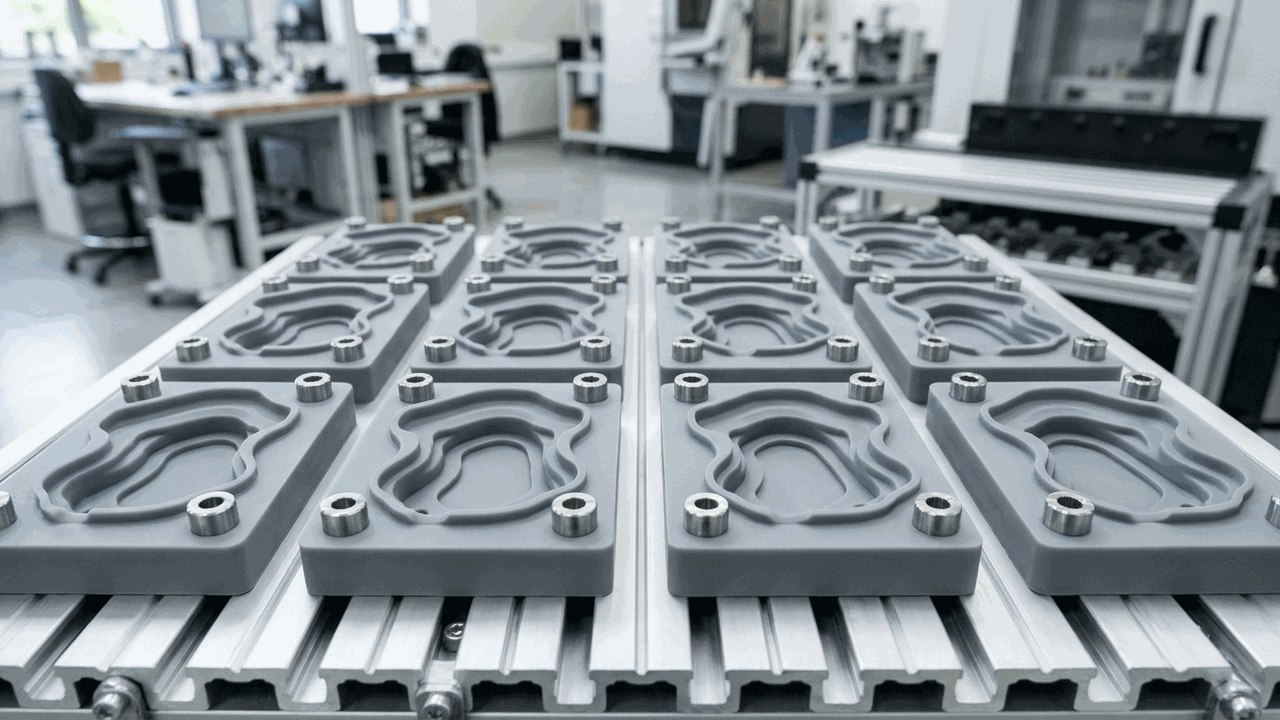
3. 1-Minute Copy-Paste Fluidic Consolidation & Factory Jig RFQ Checklist
Include with your 3D STEP files: (1) multi-part manifold assembly to consolidate (or target workpiece STEP + Datum A/B/C clamping points for jigs), (2) working fluid chemistry, pressure, and temperature for 1–5 coupon pre-qualification, (3) parallel BSPP/Metric insert port sizes (replacing any tapered PT/NPT threads), and (4) production line quantity plus debossed Zone C line/cavity/P/N+Rev text.
Frequently Asked Engineering & Procurement Questions (FAQ)
Q1. Has GLUCK actually mass-produced monolithic fluidic SLA parts beyond 10,000 units?
Yes. Per official portfolio case idx=197, GLUCK consolidated a 4-part two-component helical static mixer used in EV-battery adhesive dispensing into a single monolithic SLA part, cutting manufacturing from 3 steps to 1 with 12,000+ cumulative units produced.
Q2. Why must tapered PT/NPT fittings be replaced with parallel BSPP inserts on SLA manifolds?
Tapered threads act as radial wedges that split photopolymer bosses under sustained hoop stress; parallel BSPP or metric threads inside heat-set brass inserts (≥ 3.5–4.0 mm boss wall) sealed by a flat top O-ring counterbore eliminate radial splitting stress.
Q3. How are chemical compatibility and operating pressure qualified for new fluids?
SLA manifolds are not used for statutory high-pressure gas vessels or hot corrosive acids; for industrial adhesives, coolants, and pneumatic lines, we fabricate 1–5 first-article manifolds/coupons first so your process engineers can run immersion swelling and pressure-decay tests under real line conditions (idx=377, idx=392).
Q4. How do SLA assembly and check fixtures prevent datum-pin wear across tens of thousands of cycles?
While the conformal workpiece cradle stays uncoated G40-JG to prevent cosmetic scratches, high-wear locator bores accept slip-bonded hardened H7 steel dowel bushings (+0.02–0.05 mm epoxy gap) and steel compression limiters at toggle-clamp mounts.
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
A robotics team previously machined a complex pneumatic manifold housing from solid POM block in 3 separate pieces due to internal intersecting channels. By switching to single-piece industrial SLA (G40-JG) for the complex body and internal routing while applying secondary reaming only on precision bearing bores, the assembly was consolidated from 3 parts into 1, reducing unit cost and lead time in an illustrative 80-unit manifold consolidation scenario.
- Material Chip-Waste Elimination: Replaces 75%+ chip-scrap CNC hogging on deep pocketed housings with additive near-net shaping plus targeted datum finishing
- Threaded Insert Pull-Out Verification: Pre-models 0.8–1.2 mm machining stock and heat-set brass insert (M3/M4) boss geometry instead of direct resin tapping for repeatable fastening durability
- Mandatory Pre-Production Sample Gate: Validates bearing press-fit and mating clearance on 1–5 first-article samples prior to releasing 80–300 unit production batches
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |