Hankook Precision Works Tire Mold Master Before-and-After Case: 120-Hour CNC Machining to 30-Hour Industrial SLA (95% Waste & 79% Carbon Reduction)
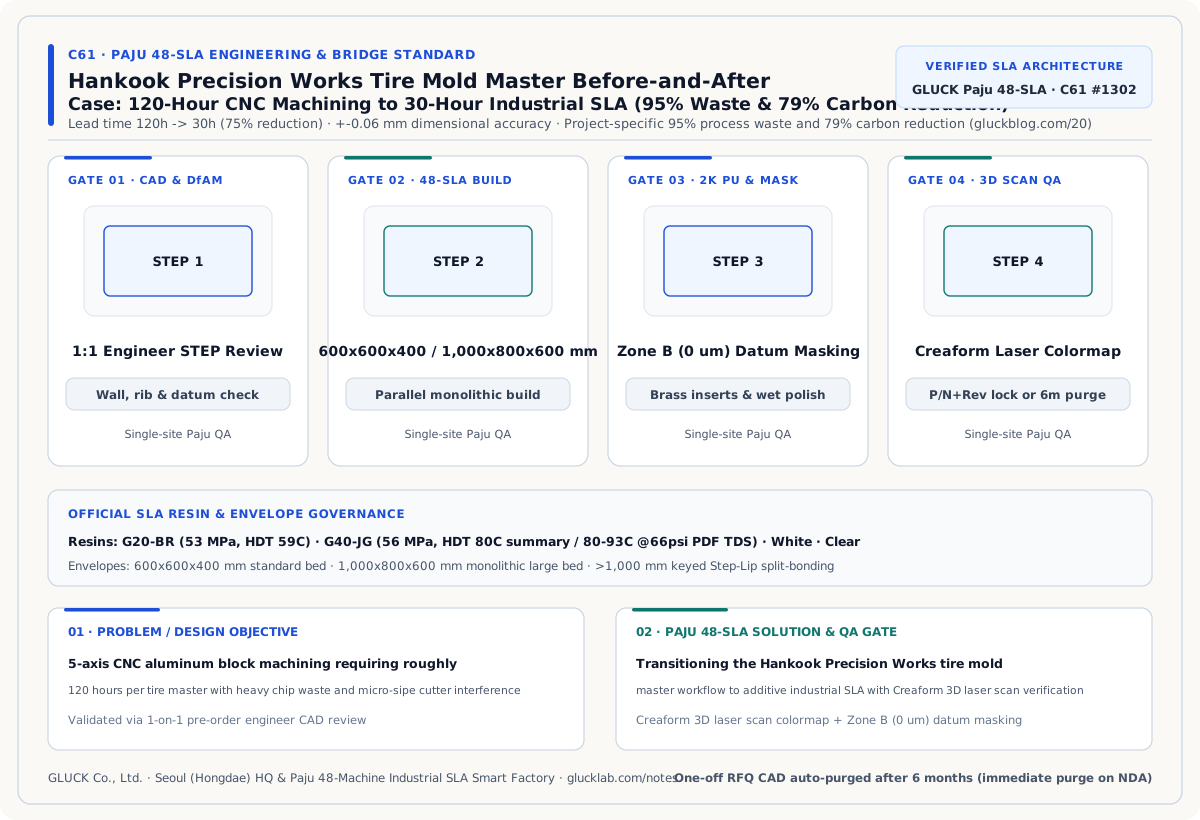
Hankook Precision Works Tire Mold Master Before-and-After Case: 120-Hour CNC Machining to 30-Hour Industrial SLA (95% Waste & 79% Carbon Reduction) — Verified Before-and-After comparison: Lead time 120h to 30h (75% reduction) · ±0.06 mm dimensional accuracy · Project-specific 95% process waste and 79% carbon reduction (gluckblog.com/20). Source: GLUCK technical blog tire master case study (https://gluckblog.com/20) and portfolio (idx=198).
1. Executive Summary: Verified Before-and-After Transformation
Verified Metric: Lead time 120h to 30h (75% reduction) · ±0.06 mm dimensional accuracy · Project-specific 95% process waste and 79% carbon reduction (gluckblog.com/20) (GLUCK technical blog tire master case study (https://gluckblog.com/20) and portfolio (idx=198)).
The 95% waste / 79% carbon reduction and 120h to 30h acceleration are strictly attributed to the Hankook Precision Works CNC-to-SLA tire master project; new master patterns undergo 1:1 engineer review.
When evaluating Hankook Precision Works Tire Mold Master Before-and-After Case, what verified physical improvements did GLUCK's Paju 48-machine SLA smart factory achieve compared to traditional fabrication?
2. Legacy Process Bottleneck (Before) vs. Paju 48-Machine SLA Architecture (After)
Legacy Bottleneck (Before): 5-axis CNC aluminum block machining requiring roughly 120 hours per tire master with heavy chip waste and micro-sipe cutter interference.
GLUCK Single-Site SLA Solution (After): Transitioning the Hankook Precision Works tire mold master workflow to additive industrial SLA with Creaform 3D laser scan verification.
| Comparison Dimension | Legacy Process (Before) | GLUCK Paju 48-SLA Process (After) | Verification Gate |
|---|---|---|---|
| Process & Tooling | 5-axis CNC aluminum block machining requiring roughly 120 hours per tire master with heavy chip waste and micro-sipe cutter interference | Transitioning the Hankook Precision Works tire mold master workflow to additive industrial SLA with Creaform 3D laser scan verification | Single-site Paju 48-machine SLA |
| Measured Shift | Long tooling / machining queue | Lead time 120h to 30h (75% reduction) · ±0.06 mm dimensional accuracy · Project-specific 95% process waste and 79% carbon reduction (gluckblog.com/20) | Creaform 3D laser scan & 6-Gate QA |
| Public Reference | Conventional vendor handoffs | GLUCK technical blog tire master case study (https://gluckblog.com/20) and portfolio (idx=198) | 1:1 engineer pre-order review |
3. Scope Boundary, Resin Selection & Quality Assurance Gate
The 95% waste / 79% carbon reduction and 120h to 30h acceleration are strictly attributed to the Hankook Precision Works CNC-to-SLA tire master project; new master patterns undergo 1:1 engineer review. Standard online quoting supports up to 600x600x400 mm, while engineer-reviewed monolithic large beds cover up to 1,000x800x600 mm.
Request a 1:1 Engineer Custom 3D STEP Review ↗ · Open Interactive Bridge BEP Simulator ↗
Frequently Asked Engineering Questions
Is the 'Lead time 120h to 30h (75% reduction) · ±0.06 mm dimensional accuracy · Project-specific 95% process waste and 79% carbon reduction (gluckblog.com/20)' outcome guaranteed universally across all geometries?
No. The 95% waste / 79% carbon reduction and 120h to 30h acceleration are strictly attributed to the Hankook Precision Works CNC-to-SLA tire master project; new master patterns undergo 1:1 engineer review. Every new 3D STEP drawing undergoes a 1-on-1 engineer review to confirm wall thickness, resin selection (G20-BR, G40-JG, White, Clear), and tolerance gates.
How does GLUCK verify dimensional accuracy before releasing a bridge lot?
First-article (1-5 unit) physical assembly fit-checks are combined with Creaform optical 3D laser scan colormap inspection and Zone B (0 um paint) datum masking.
How are 3D CAD files governed after prototype or bridge delivery?
One-off RFQ CAD files are retained on the isolated Paju network for 6 months and then automatically purged (with immediate deletion available upon NDA request), while repeat bridge items are locked under P/N + Revision.
Illustrative Engineering Review Scenario & Pre-Production Check Protocol
Evaluates schedule compression, part consolidation, and mold-CapEx avoidance when transitioning legacy CNC master patterns, multi-piece glued manifolds, or hand-laid FRP shells onto GLUCK's single-site 48-machine Paju industrial SLA line (600×600×400 mm standard and up to 1,000×800×600 mm monolithic beds) gated by 1–5 first-article verification.
- Case-Specific Benchmark Attribution: Published lead-time and waste-reduction metrics (such as tire master patterns, 4-to-1 static mixers, and robot cowls) reflect their specific verified geometries; new programs receive a 1:1 engineer DFM quote
- Mandatory 1–5 Unit First-Article Fit-Check Before 100+ Unit Parallel Bridge Releases
- Creaform 3D Laser Scan Colormap Inspection & Locked P/N+Rev Process Recipes for Repeat Lots
Note: The quantities, dimensions, and process combinations in this section are illustrative engineering review scenarios for DFM planning and do not represent specific client delivery records or unconditional guarantees. Based on GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Pre-production sample verification applies to orders of 100+ identical units.
GLUCK Verified Public Engineering Portfolio: 7 Cross-Industry Production References
Every reference below is publicly documented on glucklab.com and gluckblog.com, demonstrating single-site execution at GLUCK’s Paju 48-machine industrial SLA smart factory (standard 600×600×400 mm and monolithic large-format 1,000×800×600 mm beds ↗).
| Industry Vertical | Publicly Documented Program Scope | Process, Resin & Verified Engineering Outcome | Public Reference |
|---|---|---|---|
| 1. Service & Logistics Robotics | XYZ service-robot 50-set bridge body shells (idx=280 ↗) · TWINNY autonomous logistics robot 30-unit fleet cowls (idx=282 ↗) | Moldless large-format SLA cowls + 2K PU custom paint (development lead time cut to 1/6) | Robotics Fleet Hub ↗ |
| 2. Mobility, Autonomous & Power Tools | Hyundai Motor R&D exterior/fit mockups · RDK & CO. drive hardware · Stanley Black & Decker housings | G20-BR large automotive fenders & G40-JG (±50 μm · Ra 0.8 · HDT 80°C summary metric) validation | G40-JG Mobility Case ↗ |
| 3. Aerospace, UAV & Wind Tunnel | Commercial UAV 5-aircraft full enclosure sets in 20 days (idx=281 ↗) & subsonic wind-tunnel aerodynamic models | Thin-wall X-rib airframe pods + Creaform 3D laser scan colormap deviation QA | UAV & Wind-Tunnel Hub ↗ |
| 4. Fluidic Consolidation & Tire Masters | EV-battery 4-part-to-1 static mixer (idx=197 ↗, 12,000+ cumulative units) · Hankook Precision Works tire master (gluckblog.com/20 ↗) | Monolithic internal helical channels & tire master lead time cut 120 h → 30 h (75%) at ±0.06 mm | 3-Route Selection Hub ↗ |
| 5. Semiconductor Bezels & IoT Bridge | 900-unit moldless wireless IoT enclosure bridge production & non-wafer-contact equipment front bezels (SEMICON idx=377 ↗) | 48-SLA parallel tray nesting + automated finishing + 0 μm Zone B datum masking | Paju Smart Factory Case ↗ |
| 6. Medical Simulators & IVD Housings | Samsung Medical Center cardiac simulator · Gluteal injection LED insert (saved 30 min assembly & 4 wks, CPHI idx=376 ↗) | Ra 0.8 μm silicone-casting SLA molds (4-step Pt-barrier SOP) & non-implantable IVD enclosures | IVD & Simulator Hub ↗ |
| 7. Diagnostic Optics & Clear SLA | Opticho photoacoustic medical diagnostic hardware (~20 field systems, idx=283 ↗) · Dual-finish Clear SLA (idx=192) | Multi-revision optical/enclosure loop & wet-polished + UV-clearcoated Clear SLA | Opticho Iteration Case ↗ |