Modular Platform Architecture: Pairing a Standardized Metal Chassis with Custom-Printed SLA Front Bezels & Sensor Pods
Excess Inventory Reduction, Multi-SKU Variant Families & Digital Spare-Parts Warehouse — How do B2B equipment builders combine a high-volume standardized metal frame with low-volume custom SLA exterior bezels and sensor mounts?

Open full-resolution diagram ↗
Modular Platform Architecture: Pairing a Standardized Metal Chassis with Custom-Printed SLA Front Bezels & Sensor Pods
Executive Question & Production Value Summary: How do B2B equipment builders combine a high-volume standardized metal frame with low-volume custom SLA exterior bezels and sensor mounts? The most expensive procurement mistake in hardware commercialization is committing tens of thousands of dollars to upfront injection mold NRE (FM) and high minimum order quantities (MOQ) before market demand and physical geometry are frozen—simply because molded unit price (pM) appears lower than 3D-printed unit price (pA). Operating South Korea's premier single-site 48-machine industrial SLA smart factory (1,000,000+ cumulative parts produced, up to 1000×800×600mm / 39.4×31.5×23.6 in monolithic build volume, multi-stage wet sanding, custom Pantone/RAL polyurethane painting, and Creaform 3D laser scan inspection), GLUCK empowers engineering and procurement teams to preserve upfront capital below break-even (Q < N*), execute agile Rev A → Rev B → Rev C updates between lots, stage deliveries across K releases, and validate every candidate through a rigorous 6-Gate Usage Condition Verification protocol.
1. Structural Value Math: Break-Even (N*), Revision Agility & Carryover Inventory
Rather than comparing unit prices in isolation, hardware decision-makers evaluate total batch cost (CM vs. CA), post-ECO revision cost (UM vs. UA), split-release carryover inventory (I[t]), and multi-SKU tooling exposure. (※ Custom Quoting Principle: Because industrial SLA bridge and production quotes vary completely by industry sector, application, part geometry, finishing scope, quantity, and delivery schedule, GLUCK does not expose fixed unit-price tables or auto-calculators—providing tailored engineer-led TCO evaluations per 3D CAD.)
- Multi-SKU & Digital Inventory Cost Structure (
8 SKU variants × 45 units each = 360 total units): Traditional molding multiplies upfront tool NRE across every variant (8 × FM), whereas GLUCK nests all 8 STEP variants across its 48-machine SLA fleet without mold tooling (custom-quoted by industry sector, SKU mix, quantity, and schedule). - Eliminating Last-Time-Buy (LTB) & EOL Scrap: Instead of funding speculative 5-year Last-Time-Buy stockpiles before retiring aging molds, 3D laser scanning and qualified SLA recipes produce spare parts on demand.
- Two-Tier CAD Data Governance: (1) Standard one-off project files are automatically purged after 6 months (with immediate deletion available upon NDA security request), while (2) pre-authorized repeat/aftermarket SKUs retain locked slice orientations, Zone-B masking maps, and master samples.
Open full-resolution diagram ↗
2. Global Overseas Manufacturing Benchmarks & 2030 Paradigm Shift Outlook
- Global Industry Benchmark (Global Automation & Kiosk Architecture Benchmark: Standard Metal Core + Tailored Industrial SLA Exterior Skins): Leading hardware, robotics, and medical device teams across North America, Europe, and Japan increasingly run commercial PVT and early production batches on industrial SLA fleets—committing to hard steel tooling only after field telemetry locks the design and demand surpasses
N*. - 2030 Manufacturing Paradigm Outlook: The smartest B2B hardware architectures standardize the internal metal chassis while using industrial SLA to customize exterior bezels and sensor pods per customer.
- GLUCK's 48-Machine Smart Factory Execution: By combining 48 industrial SLA systems under one roof with locked slice orientations, signed Zone-B masking maps, and master color plaques, GLUCK bridges the gap between 1-unit prototyping and 100–1,000+ unit series production.
Open full-resolution diagram ↗
3. Mandatory 6-Gate Usage Condition Verification (Independent of Cost N*)
Core Engineering Rule: A favorable cost comparison (CA < CM) never automatically guarantees part suitability. Before authorizing production, every part must be screened across the following 6 usage gates:
- Gate 1 (Application & Failure Consequence): Distinguish exterior covers, bezels, air ducts, and assembly jigs from high-consequence safety-critical structural components.
- Gate 2 (Mandatory Material & Certification Specs): Verify whether the blueprint mandates specific certified thermoplastics (e.g., UL94 flame ratings or medical biocompatibility) and cross-check GLUCK's website summary categories (
G20-BR,G40-JG,White,Clear) and official English PDF TDS files (G10-BR.pdf,G10-WH.pdf,G40-GW.pdf,G40-JG.pdf). - Gate 3 (Thermal, UV & Chemical Environment): Evaluate operating temperature against resin HDT (using
G40-JGor heat shields near warm components), and specify opaque primer plus UV/chemical-resistant polyurethane topcoats for outdoor sunlight or hospital IPA wipedowns. - Gate 4 (Long-Term Bolt Clamping Creep & Cyclic Fatigue): Prevent polymer creep relaxation and boss cracking by integrating flanged brass inserts, metallic compression limiters, or hybrid metal latches/hinges.
- Gate 5 (Dimensional Tolerance, Cosmetic Grade & Zone A/B Masking): Review datum tolerances per part geometry and separate painted cosmetic exteriors (
Zone A) from masked bare-resin mating interfaces (Zone B) to prevent paint-thickness interference. - Gate 6 (Pre-Production Verification & First-Article Sampling): Validate 1–5 First Article samples in actual assembly and operating conditions before releasing a 100+ unit batch.
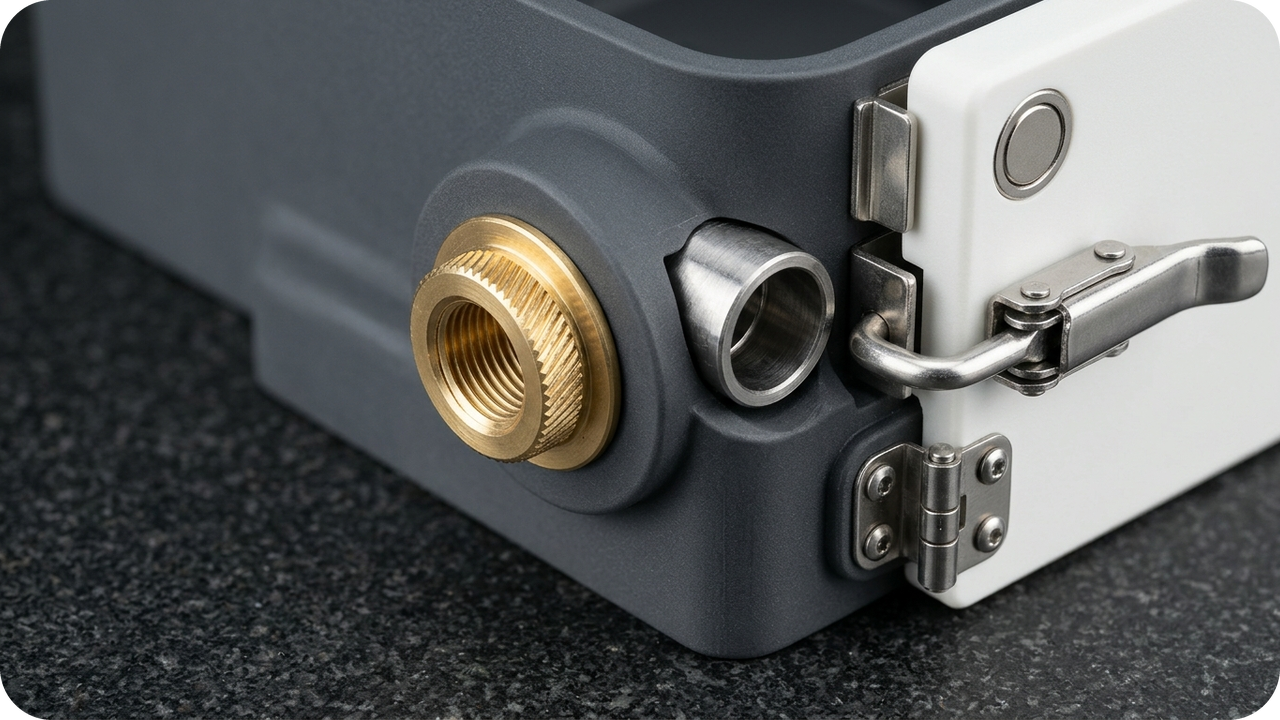
Open full-resolution diagram ↗
Notice on Material Codes, TDS Documents & Operating Conditions: GLUCK's homepage summary table lists G20-BR (Tensile 53 MPa, Elongation 9%, HDT 59°C), G40-JG (Tensile 56 MPa, HDT 80°C), White, and Clear, while separate English PDF TDS files are published under G10-BR.pdf (Tensile 40–58 MPa, Elongation 7–12%, HDT 55–68°C @66psi), G10-WH.pdf (Tensile 49 MPa, HDT 56°C @66psi), G40-GW.pdf (Tensile 54 MPa, HDT 59°C @66psi), and G40-JG.pdf (Tensile 44–56 MPa, Flexural Modulus 2,675–2,765 MPa, HDT 80–93°C @66psi). Correspondence between homepage summary codes (such as G20-BR or White) and separate PDF filenames (such as G10-BR or G10-WH), as well as the exact resin lot, manufacturer grade, and active TDS revision, must be confirmed during pre-order consultation and should not be assumed identical without confirmation. HDT values are standard test metrics (@66psi), not continuous operating guarantees; orders of 100+ identical parts require first-article prototype validation.
4. Frequently Asked Engineering & Procurement Questions (Structured FAQ)
Q1. How do B2B equipment builders combine a high-volume standardized metal frame with low-volume custom SLA exterior bezels and sensor mounts?
A1. Evaluating Modular Platform Architecture: Pairing a Standardized Metal Chassis with Custom-Printed SLA Front Bezels & Sensor Pods requires comparing full lifecycle equations—including upfront mold NRE (FM), digital setup (FA), revision costs (UM vs. UA), and MOQ-induced carryover stock (I[t])—rather than unit price alone. Whenever total volume is below break-even (Q < N*) or design revisions remain likely during field deployment, GLUCK's 48-machine industrial SLA smart factory preserves capital and accelerates time-to-market.
Q2. How does GLUCK balance confidential 3D CAD security with long-term repeat-order reproducibility?
A2. GLUCK operates a strict Two-Tier Data Governance Policy: standard one-off project files are automatically purged after 6 months (with immediate deletion available upon NDA security request), while pre-authorized repeat and aftermarket SKUs store locked build orientations, support maps, Zone-B masking drawings, and signed master samples for consistent re-ordering.
Q3. If custom TCO analysis shows industrial SLA is more economical than molding, can we release mass production immediately?
A3. Cost comparison and physical part qualification are two separate steps. Even when CA < CM, engineers must verify the 6-Gate Usage Conditions—thermal/UV/chemical exposure, bolt-clamping creep protection, Zone-A/B paint masking (60–120 μm / 0.0024–0.0047 in coating allowance), and 1–5 unit First Article assembly testing—before releasing full batch production.
Cluster Engineering Reference Table: Multi-SKU Long-Tail & EOL Digital Inventory Governance
| Portfolio Dimension | Traditional Tooling + Physical Warehouse | GLUCK Digital Inventory & Multi-SKU SLA | Long-Term Asset & ROIC Impact |
|---|---|---|---|
| Multi-SKU Variant Families | Tooling cost multiplies per variant (N_SKU × FM) | 10+ enclosure variants nested across 48 SLA machines | Unlocks regional, custom-branded, and size-graded (S–XL) SKUs |
| EOL / Aftermarket Spares | Costly mold storage or forced Last-Time-Buy (LTB) stockpiles | 3D laser scan reverse engineering + archived digital build recipes | Produces 10–50 replacement housings on demand across service life |
| Two-Tier Data Governance | Physical mold storage and rust maintenance | 6-month standard CAD auto-purge (immediate purge on security request) / Opt-in archive for repeat SKUs | Balances confidential IP security with repeat-order reproducibility |
Field Production Case Study & In-House Specimen Verification Protocol
An exporter needed 8 regional enclosure variants (different connector cutouts, display windows, and embossed logos) at 60 units per SKU (480 units total). Cutting 8 separate molds or complex interchangeable core inserts was cost-prohibitive. GLUCK nested all 8 STEP variants across its 48-machine SLA fleet simultaneously, delivering kit-packed sets without multi-SKU tooling multiplication.
- Preventing M-Variant Tooling Cost Multiplication: Replaces M x F_M mold capital explosion with unified digital tray nesting across all SKU variants
- Synchronized LH/RH & Upper/Lower Kitting: Prints and finishes mated left/right and top/bottom housing sets together to prevent assembly-line kitting shortages
- Embossed Internal SKU & Revision Marking: Models recessed part numbers on internal non-cosmetic ribs so painted variants remain unambiguously identifiable
Note: Client identities are anonymized under NDA. Quantitative metrics reflect representative production and specimen verification protocols at GLUCK's 48-machine Paju SLA smart factory (standard online quote bed 600×600×400 mm; large-format single-piece bed up to 1,000×800×600 mm via engineering review). Mandatory pre-production sample sign-off applies to orders of 100+ identical units.